Get 50% OFF All Premium 3D & STL Models!
“`html
The world of 3D modeling and printing is rich with possibilities, from crafting intricate printable car models to designing functional prototypes. As you venture into this exciting domain, you’ll inevitably encounter various 3D file formats. Among the most common are STL, OBJ, and FBX. But which one is the undisputed champion when it comes to preparing your digital creations for the tangible reality of 3D printing? Understanding the nuances of each format is crucial for ensuring successful prints, avoiding frustrating errors, and achieving the high-quality results you envision. This comprehensive guide will demystify these formats, break down their technical structures, and provide clear guidance on selecting the best option for your specific 3D printing needs. We’ll explore their strengths, weaknesses, and how they interact with slicing software, mesh repair tools, and your 3D printer itself. Prepare to gain the knowledge that will elevate your 3D printing workflow from frustration to flawless execution.
When it comes to 3D printing, the STL (Standard Tessellation Language or Stereolithography) format reigns supreme. Its widespread adoption by slicers and 3D printers is not accidental; it stems from its fundamental design, which is inherently optimized for representing surfaces suitable for additive manufacturing. An STL file describes the surface geometry of a 3D object using a collection of connected triangles. Each triangle is defined by the coordinates of its three vertices and a normal vector, which indicates the outward-facing direction of the surface. This simple, yet effective, approach makes it incredibly straightforward for slicing software to interpret the geometry and generate toolpaths for the printer.
The core of an STL file is its tessellation. This means that any complex curved surface is approximated by a mesh of small, flat triangles. The more triangles used, the smoother and more detailed the approximation will be. However, this also leads to larger file sizes. The normal vector associated with each triangle is vital for ensuring the “watertightness” or manifold integrity of the model. A manifold model is one that has no holes or self-intersections, representing a single, solid volume. Slicers rely on these normals to determine which side of the triangle is “inside” and which is “outside” the object. Incorrectly oriented normals can lead to slicing errors, missing sections in your print, or inversion of parts of your model.
Key characteristics of STL:
The simplicity of STL is its greatest strength in the 3D printing context. Slicing software, such as Cura or PrusaSlicer, can efficiently process these files. They analyze the arrangement of triangles to determine the outer shell, inner structures, and any necessary support material. For instance, when you download a high-quality printable car model from a marketplace like 88cars3d.com, you’ll most likely find it provided in STL format because it’s the most universally compatible. This broad compatibility minimizes the technical hurdles for users, allowing them to focus on print settings and quality. Even with complex organic shapes, the triangulation process, when done correctly in modeling software, ensures that the slicer has a clear definition of the object’s boundaries, crucial for generating accurate G-code.
For straightforward 3D printing applications where color, texture, and complex material properties are not primary concerns, STL is the go-to format. This includes:
The primary consideration when using STL is the quality of the mesh. A poorly generated STL with holes, non-manifold edges, or inverted normals will cause significant problems during slicing and printing. Fortunately, tools like Meshmixer, Blender, or Netfabb can be used to repair and optimize STL files before printing.
The OBJ (Object) file format offers a more comprehensive representation of 3D data compared to STL. Developed by Wavefront Technologies, OBJ files can store not only the geometric information of a model but also crucial data like color, texture maps, and material definitions. This makes it a popular choice in the broader 3D graphics industry, particularly for animation, game development, and rendering. For 3D printing, OBJ’s ability to retain color and material information can be beneficial, especially for multi-color or multi-material printing scenarios, although direct slicer support for these features can vary.
An OBJ file typically consists of several key components. It defines vertices (points in 3D space), texture coordinates (UVs, which map textures onto the model’s surface), normal vectors for each vertex (for smoother shading), and faces (which can be triangles or polygons). Crucially, OBJ files can reference external material and texture files (often with MTL and image extensions, respectively), allowing for rich visual properties. This is a significant advantage over STL, which is purely geometric.
Key characteristics of OBJ:
For 3D printing, the OBJ format’s primary advantage lies in its potential for more detailed modeling and, importantly, its ability to convey color information. If you’re using a multi-color FDM printer or a resin printer capable of CMYK printing, an OBJ file with associated color data could theoretically streamline the process. However, the practical implementation is complex. Most slicers will primarily focus on the geometry of the OBJ file, often discarding color information unless specifically designed to handle it. This means that even if you have a beautifully colored OBJ model, you might still need to assign colors within the slicer for multi-color prints.
Furthermore, the polygonal nature of OBJ (supporting quads and n-gons) can sometimes result in cleaner geometry compared to heavily triangulated STLs, especially when exporting from CAD software that uses NURBS surfaces. This can lead to smoother curves and less “faceted” appearance before slicing.
OBJ is a strong contender when:
As with STL, ensuring the OBJ file is manifold and free of errors is critical. Software like Blender or Meshmixer can be used to check and repair OBJ files, ensuring they are suitable for slicing.
The FBX (Filmbox) file format, developed by Autodesk, is another powerful contender in the 3D file format landscape. It is widely used in the entertainment industry, particularly for game development and animation, due to its comprehensive support for a vast array of 3D data. FBX can store detailed scene information, including geometry, materials, textures, skeletal animation, lighting, and cameras. While its primary strength lies in animation pipelines, its geometric and material data can be relevant for certain advanced 3D printing scenarios, especially when transferring complex scenes or models between different software packages.
FBX is designed for robust interoperability between different applications. It supports various data types, including:
The ability to embed textures directly within the FBX file, rather than relying on external references like OBJ, can simplify asset management. However, this also contributes to potentially larger file sizes.
For most standard 3D printing applications, the advanced features of FBX, such as animation data, are irrelevant. Slicing software typically ignores these elements and focuses solely on the geometric mesh. Therefore, when you import an FBX file into a slicer, it often behaves similarly to an OBJ file, extracting the geometry and potentially any associated material or color information that the slicer can interpret. The main benefit of FBX for printing might arise if you are exporting from a complex animation or game design environment and want to maintain the integrity of the model’s geometry and UV mapping, which can be crucial if you plan to use detailed textures or decals on your printed object.
However, FBX support in slicing software is not as universally guaranteed as STL. While many modern slicers can import FBX, occasional compatibility issues or unexpected interpretations of the mesh data can occur. When dealing with intricate models, such as those found on 88cars3d.com, ensuring the FBX is clean and manifold is paramount.
FBX is most beneficial when:
It’s important to note that for simple geometric models intended solely for printing, FBX might be overkill, and its complexity could introduce unforeseen issues. Always verify that your chosen slicer fully supports FBX import and handles its geometric data as expected.
When the dust settles, the choice between STL, OBJ, and FBX for 3D printing hinges on your specific needs and the capabilities of your tools. STL remains the undisputed king of compatibility and simplicity for most 3D printing tasks. Its triangle-based structure is directly interpretable by virtually all slicing software, making it the most reliable format for ensuring your model can be translated into printable instructions. The trade-off is its lack of any data beyond raw geometry. If your goal is simply to print a watertight model, STL is usually the safest and most efficient choice.
OBJ steps up by offering more data, including color and material information, and supports more flexible polygon types. This makes it a better choice if you’re working with models that have textures or if you plan to engage in multi-color printing, provided your slicing software and printer can handle the additional data. However, the reliance on external MTL and texture files can sometimes complicate file management.
FBX is the most feature-rich, designed for complex scene data and animation. While it can store geometry and material information, its primary strengths lie outside the typical 3D printing workflow. For printing, its value is mainly in its ability to transfer complex models from specific software pipelines, potentially preserving UV layouts and embedded textures. However, its complexity can also lead to compatibility issues with some slicers, and its advanced features are often ignored during the slicing process.
Regardless of the chosen format, the **most critical factor for successful 3D printing is the integrity of the mesh**. Whether you download a model from a platform like 88cars3d.com or create your own, it must be “watertight” (manifold). This means there should be no holes, no inverted faces, and no self-intersecting geometry. Common tools for checking and repairing meshes include:
For STL, focus on ensuring all faces have consistent normal directions. For OBJ and FBX, pay attention to non-manifold edges and holes, especially if you intend to leverage color or material data. Always perform a mesh check before sending a file to your slicer.
Once you have a clean, watertight 3D model in your chosen file format, the next critical step is slicing. The slicer software acts as the interpreter, converting your 3D model into a series of layer-by-layer instructions (G-code) that your 3D printer can understand. The settings you choose here will profoundly impact the quality, strength, and print time of your final object. While slicers handle STL files most directly, they can also process OBJ and FBX by extracting the necessary geometric data.
One of the most significant settings is **layer height**. A smaller layer height (e.g., 0.08mm or 0.12mm) results in finer detail and smoother curves, but significantly increases print time. A larger layer height (e.g., 0.2mm or 0.3mm) prints much faster but will produce more visible layer lines. For highly detailed printable car models, you might opt for a lower layer height. For less detailed parts or when speed is paramount, a higher layer height is acceptable.
Print speed should generally be reduced when using smaller layer heights or printing intricate details to ensure accuracy and adhesion. Common FDM speeds range from 40 mm/s for high-quality prints to 80 mm/s or more for faster, less detailed prints. For resin printing, layer heights are typically much smaller (e.g., 0.025mm to 0.05mm), and exposure times are critical rather than print speed in the FDM sense.
The infill dictates the internal structure of your print. **Infill density** (e.g., 10-25% for most models) affects the part’s strength, weight, and material consumption. Higher density means a stronger, heavier, and longer print.
The **infill pattern** also plays a role. Common patterns include:
For display models, lower infill densities and simpler patterns are often sufficient. For functional parts, choose patterns like gyroid or cubic with higher densities.
Overhanging features and bridges in your 3D model cannot be printed in mid-air. Slicers automatically generate **support structures** to hold these sections during printing. Key settings include:
Proper support generation and removal are crucial for achieving clean prints, especially for detailed models with complex geometries. Experiment with different support settings to find the best balance between print success and ease of post-processing.
The journey doesn’t end when the print is finished. Post-processing is often a necessary step to achieve a professional-looking final product, whether you’re assembling a detailed car model or finishing a functional prototype. The techniques you employ will depend on the printing technology (FDM vs. resin), the material used, and your desired aesthetic.
The first step is often the careful removal of support structures. This can be done with pliers, flush cutters, or specialized tools. For resin prints, supports are typically removed after washing and before final curing. Be gentle to avoid damaging the model’s surface. After support removal, you’ll likely be left with small marks or blemishes.
Sanding is a common technique to smooth out layer lines and remove imperfections. Start with a coarser grit sandpaper (e.g., 150-220 grit) and progressively move to finer grits (e.g., 400, 800, 1000+ grit) for a smooth finish. For FDM prints, consider using a rotary tool with sanding attachments for larger areas. For resin prints, sanding can be done wet to reduce dust and achieve a smoother surface.
For an even smoother finish, especially on FDM prints, you can use fillers like wood filler, Bondo, or specialized 3D printing putties to fill gaps and layer lines. After filling, apply a primer coat. Primer helps to reveal any remaining imperfections and provides a uniform surface for painting.
Painting can transform a basic plastic print into a realistic replica. Use acrylic paints, spray paints, or airbrushing. For detailed models like those from 88cars3d.com, consider using fine brushes for intricate details like trim, lights, and emblems. Techniques like dry brushing can highlight details, while washes can add depth and realism.
Many complex models, especially larger or multi-part car models, will require assembly. Ensure you have the right adhesive for your material. Super glue (cyanoacrylate) works well for most plastics, while epoxy adhesives offer stronger bonds for larger or stressed parts. For FDM prints, specialized plastic cements can fuse the layer lines for a stronger, more seamless bond. Test fit parts before applying adhesive to ensure proper alignment.
Navigating the world of 3D file formats can seem daunting, but understanding the core differences between STL, OBJ, and FBX empowers you to make informed decisions for your 3D printing projects. For the vast majority of 3D printing applications, especially when downloading models from marketplaces like 88cars3d.com, **STL remains the most reliable and universally compatible format**. Its simplicity ensures broad support across slicing software and printers, minimizing potential compatibility issues. If you require color or texture information, OBJ offers a step up, but always verify your slicer’s capabilities.
FBX, while powerful, is generally overkill for standard 3D printing and may introduce unnecessary complexity. The true key to successful printing, regardless of file format, lies in **mesh integrity**. Always ensure your files are watertight and free of errors before slicing. Mastering your slicer’s settings—layer height, print speed, infill, and supports—is equally crucial for achieving high-quality results. Finally, don’t underestimate the impact of post-processing; sanding, filling, priming, painting, and careful assembly can elevate your printed models from raw output to stunning creations.
By understanding these file formats and the associated printing workflows, you can confidently tackle any 3D printing project, from intricate automotive replicas to functional prototypes. Happy printing!
“`
Texture: Yes
Material: Yes
Download the Toyota MRS-007 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Porsche 911 Turbo S 2024 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $20

Texture: Yes
Material: Yes
Download the Pontiac Solstice 2009 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Mini Cooper Countryman 2025 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $29.9
Texture: Yes
Material: Yes
Download the Mercedes C Classe 2012 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $19.9
Texture: Yes
Material: Yes
Download the Mercedes-Benz S65 AMG 2018 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $19.9
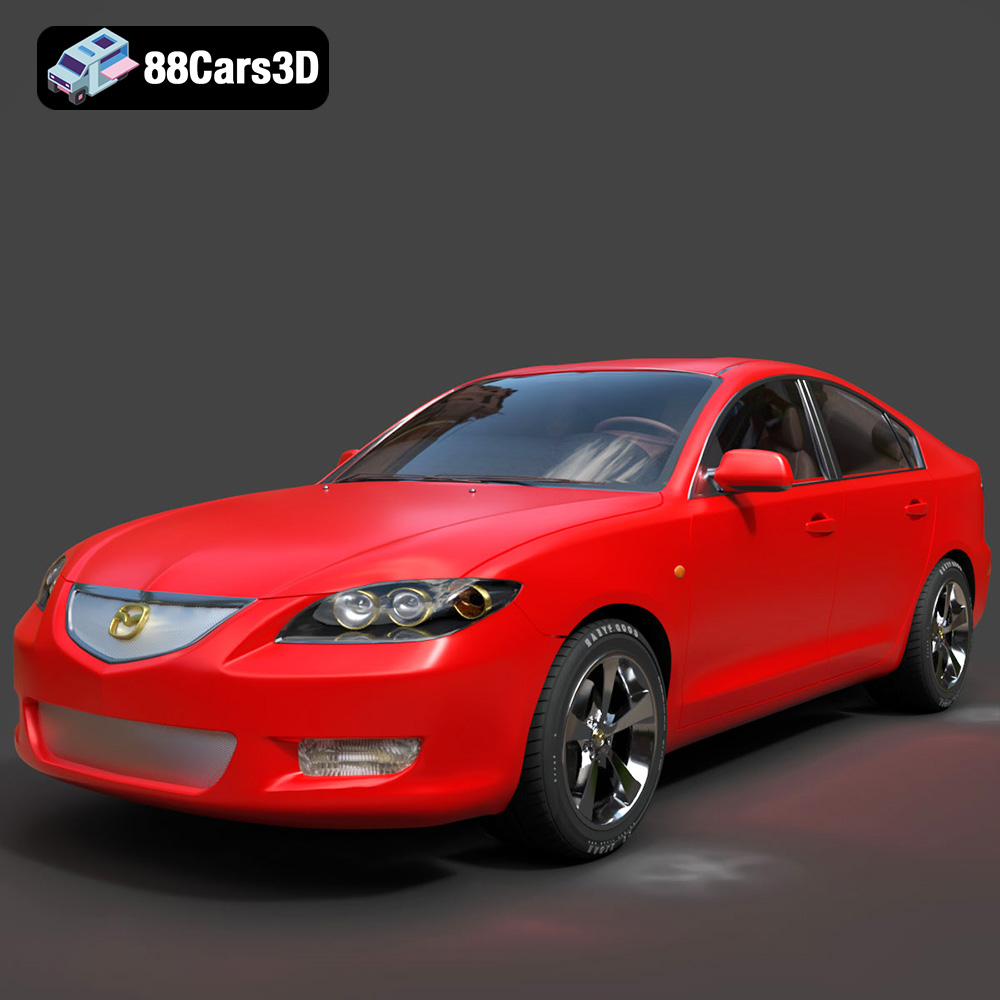
Texture: Yes
Material: Yes
Download the Mazda 3 Sedan 2004 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Martin Rapide 2011 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $20.9
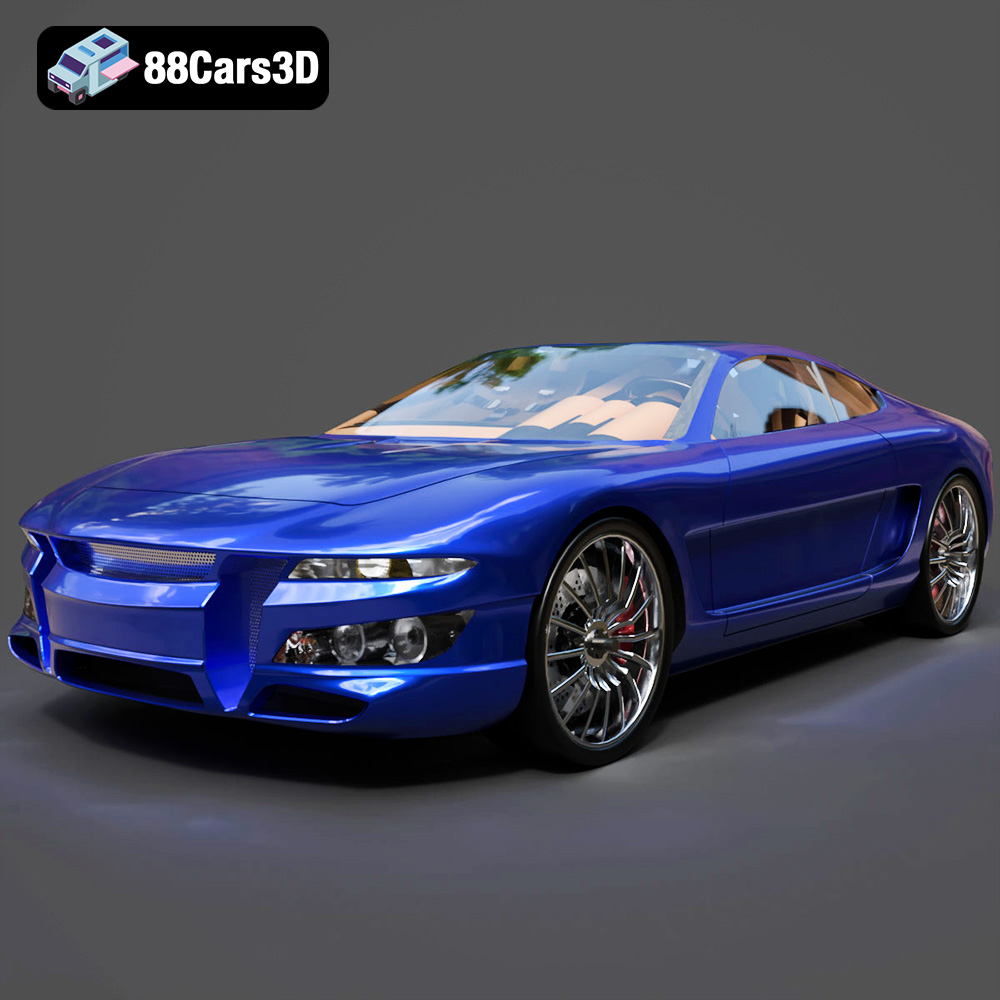
Texture: Yes
Material: Yes
Download the Car Tasergal 005 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10
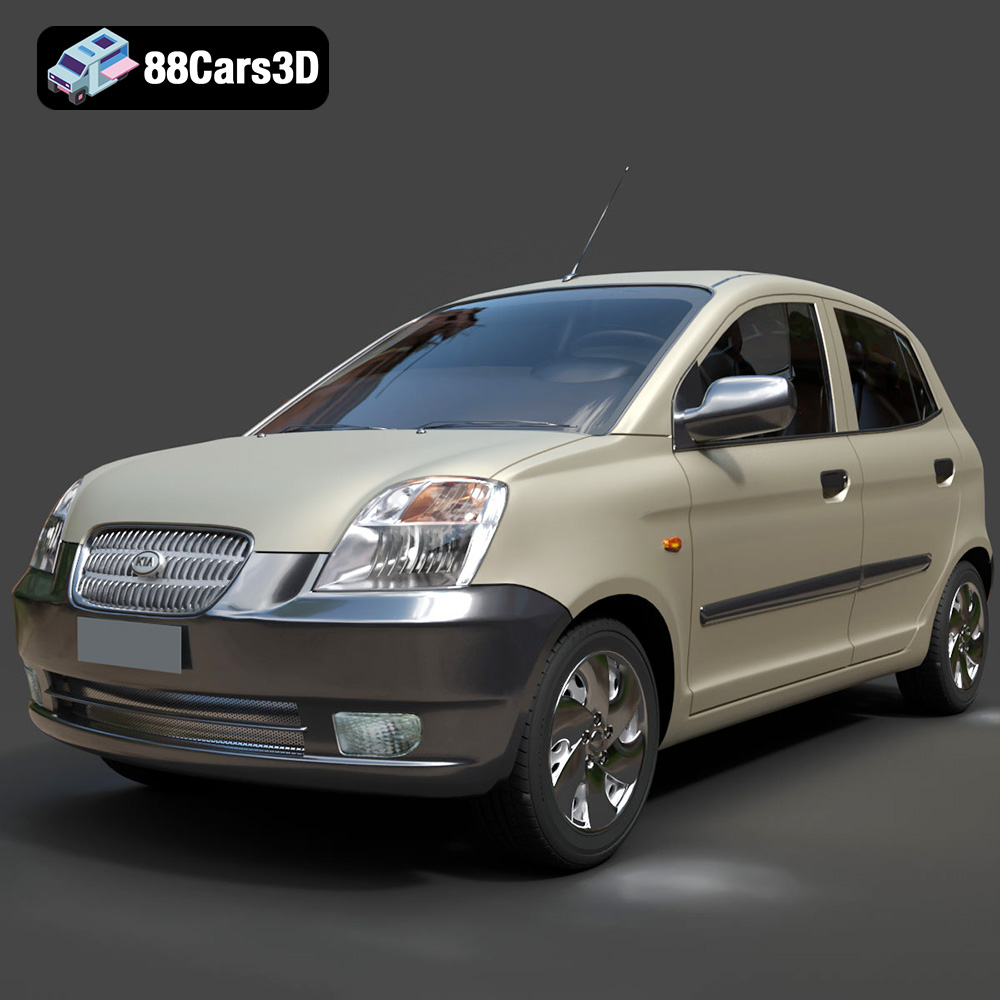
Texture: Yes
Material: Yes
Download the Kia Picanto 2024 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $15.99

