Get 50% OFF All Premium 3D & STL Models!
“`html
The world of 3D printing is an exciting frontier for hobbyists, engineers, and automotive enthusiasts alike. At 88cars3d.com, we’re passionate about bringing iconic vehicles to life through high-quality, printable STL files. However, translating intricate designs – especially those with challenging overhangs, fine details, and delicate features found in detailed car models – into successful physical prints can be daunting. Overcoming print failures is a rite of passage for many in the additive manufacturing community. This guide will equip you with the knowledge and techniques to tackle complex geometries head-on, ensuring your 3D prints are as detailed and perfect as the original digital models. We’ll delve into the nuances of STL file preparation, advanced 3D printer settings, sophisticated slicing strategies, and the crucial role of support structures. Whether you’re using FDM or resin technology, by the end of this article, you’ll have a robust understanding of how to achieve stunning results and minimize those frustrating print failures.
The STL file format, standing for Stereolithography or Standard Tessellation Language, is the de facto standard for 3D printing. It describes the surface geometry of a 3D object using a mesh of triangular facets. While simple and universally compatible, its tessellated nature can introduce complexities when dealing with curved surfaces and intricate details common in automotive models. The resolution of the STL mesh directly impacts the print quality; a low-resolution STL will result in a visibly faceted object, while an excessively high-resolution one can create massive file sizes and processing challenges for slicers. For complex geometries, the arrangement and orientation of these triangles are paramount. Poorly defined or non-manifold meshes – where edges are shared by more than two triangles, or where triangles intersect improperly – are a primary source of printing errors. Understanding that your STL is essentially a collection of interconnected triangles helps in diagnosing issues like gaps in the print, surface imperfections, and slicing errors. When downloading models from marketplaces such as 88cars3d.com, the quality of the underlying mesh is crucial. Reputable sources ensure their STL files are manifold and optimized for printing, minimizing initial geometry-related headaches.
A “manifold” mesh is akin to a closed surface, with no holes, tears, or self-intersections. Think of it as a perfectly sealed balloon. Non-manifold geometry arises when this integrity is compromised. Common issues include:
These errors can cause slicers to misinterpret the model, leading to failed prints, missing sections, or incorrect toolpaths. Specialized software like Meshmixer, Blender, or Netfabb are invaluable for diagnosing and repairing these issues. Automatic repair functions can often fix simple problems, but manual intervention might be needed for more complex mesh distortions. Always perform a mesh check and repair before proceeding to slicing.
The level of detail in your 3D print is directly related to the STL’s resolution – how many triangles are used to represent the model’s surfaces. A higher resolution means more triangles, smoother curves, and finer details. However, this comes at a cost: larger file sizes and longer processing times for your slicer. For extremely complex models with very fine features, like intricate grilles or emblems on a car model, a higher resolution STL is necessary. Conversely, for simpler shapes or larger-scale prints, a lower resolution might suffice and result in more manageable file sizes. Finding the right balance is key. Platforms like 88cars3d.com often provide models in various resolutions or clearly state the recommended settings for optimal detail. Experimentation is often required; check if your slicer can preview the imported mesh and look for any obvious faceting that would be unacceptable in the final print.
The slicer software is your bridge between the digital STL file and the physical 3D printer. For complex models, default slicing settings are rarely sufficient. Mastering advanced slicing techniques is crucial for mitigating failures. This involves meticulously adjusting parameters related to layer height, print speed, retraction, cooling, and, most importantly, support structures. The goal is to create toolpaths that respect the model’s geometry, minimize stress points during printing, and facilitate easy removal of any necessary supports without damaging the underlying print. Understanding how each setting influences the printing process allows for fine-tuning to match the specific demands of a complex car model, ensuring that delicate spoilers, thin pillars, or intricate interior details are reproduced faithfully.
Layer height is one of the most significant factors influencing print quality and time. A smaller layer height (e.g., 0.1mm) produces smoother surfaces and captures finer details, which is essential for complex car models with smooth curves and sharp edges. However, it dramatically increases print time as the printer must lay down many more layers to complete the object. Conversely, a larger layer height (e.g., 0.2mm or 0.3mm) speeds up printing considerably but can result in visible layer lines and a loss of fine detail. For parts of a complex model that require high fidelity, consider using a smaller layer height. For less critical areas or prototypes, a larger layer height can save significant time. Some slicers allow for adaptive layer heights, where the layer height automatically adjusts based on the model’s geometry – smaller layers for steep slopes and details, larger layers for vertical sections. This is an excellent compromise for complex shapes, optimizing both quality and print duration.
The infill is the internal structure of your print, providing support and determining the object’s strength and weight. For complex models, the infill plays a role in preventing internal collapse and supporting overhangs from below. Standard infill patterns like Grid, Lines, or Cubic offer good structural integrity. For highly detailed parts where internal support might be crucial for specific overhangs, consider patterns like Gyroid, which offers good strength in multiple directions and can sometimes reduce the need for extensive external supports by providing internal anchoring points. Infill density is also critical. While 10-20% is common for display models, complex geometries with significant overhangs might benefit from slightly higher infill (e.g., 25-30%) in specific areas to provide better support from below. However, excessive infill increases print time and material usage. It’s often more effective to use specialized support structures than to rely solely on high infill density for challenging overhangs.
Printing complex geometries often requires slower print speeds. High speeds can lead to ringing artifacts, poor layer adhesion on overhangs, and skipped steps, especially with intricate details. Reducing the overall print speed, particularly for outer walls and overhangs, can significantly improve quality. A common starting point for detailed prints is around 40-50 mm/s. Equally important is adequate cooling. Good cooling solidifies newly deposited plastic quickly, allowing it to hold its shape and preventing sagging on overhangs and bridges. Ensure your 3D printer’s part cooling fan is functioning optimally. For materials like ABS or ASA, which are prone to warping and require slower speeds, managing cooling becomes a balancing act; too much can cause delamination, too little leads to drooping. Fine-tuning fan speed based on the material and the specific geometry being printed is essential.
Support structures are arguably the most critical element when printing complex geometries, particularly models with significant overhangs and bridges, like the detailed bodywork, spoilers, and undercarriages of car models. Without proper supports, these features will sag, deform, or fail entirely. The goal is to create structures that are strong enough to hold the overhanging parts during printing but are also easy to remove cleanly afterward, leaving minimal marks on the finished model. This involves understanding the different types of supports, their placement, density, and interface settings. Choosing the right support strategy can be the difference between a perfect print and a frustrating failure. Platforms like 88cars3d.com often provide models that have been designed with support considerations in mind, but understanding how to generate and optimize them yourself is a vital skill.
Standard, vertical supports are the most common type. They are generated as pillars extending from the build plate or other parts of the model directly beneath the overhang. While effective, they can sometimes be difficult to remove from intricate surfaces and may leave more scarring. Tree supports, a more advanced option available in slicers like Cura and PrusaSlicer, are generated as branching structures that reach out to support overhangs. They typically use less material, print faster, and are often easier to remove from detailed surfaces because they make contact at fewer points. Tree supports can be configured to be more flexible or rigid and can be angled to avoid critical features. For complex car models with delicate details like mirrors or spoilers, tree supports are often the preferred choice due to their minimal contact points and ease of removal.
The “overhang angle threshold” is a key setting. It tells the slicer which angles are considered overhangs that require support. A typical threshold is around 45-60 degrees. Anything steeper than this angle will require support. For highly detailed car models, you might need to adjust this threshold. For example, a subtle curve on a car door might require support if it exceeds the threshold, even if it doesn’t look like a severe overhang. Manually adding support blockers or enabling “support only on build plate” can help prevent supports from attaching to delicate model features where removal would be difficult. Conversely, sometimes you need to force supports in specific locations to prop up a particularly challenging feature. Careful placement is crucial; avoid placing supports where they will obscure fine details or be impossible to reach for removal.
The interface between the support structure and the actual model is critical for both print success and post-processing. Support interface settings control this layer. Options like “Support Roof” and “Support Floor” create denser, flatter layers at the top and bottom of the support structure, providing a more stable surface for the overhang to print on and a cleaner surface where the support attaches to the model. Adjusting the “Support Interface Density” and “Support Interface Pattern” can make a significant difference. A slightly denser interface can create a stronger bond, but too dense makes removal difficult. Experiment with settings like “Zig-Zag” or “Concentric” for the interface pattern. The “Z Distance” (the gap between the support and the model) is also vital; a larger gap makes removal easier but increases the risk of the overhang sagging. A smaller gap (e.g., 0.1-0.2mm for FDM) can improve overhang quality but requires more careful removal.
How you position your 3D model on the print bed, known as print orientation, is a fundamental decision with significant implications for print success, particularly for complex geometries. The orientation affects the number and angle of overhangs, the surface area in contact with the build plate, and the distribution of stresses during printing. Proper bed adhesion ensures the first layers stick firmly to the build surface, preventing warping and detachment, which are common failure points. For intricate car models, choosing the right orientation and ensuring excellent bed adhesion are paramount to capturing delicate features and achieving a stable, successful print from start to finish.
For complex car models, there’s rarely a single “best” orientation. You need to consider several factors:
Using your slicer’s preview function to examine the orientation and visualize supports is crucial. Experiment with different rotations to find the orientation that best balances these factors for your specific model and printer.
A failed print often starts with poor bed adhesion. For complex models with potentially small initial contact areas, this risk is amplified.
The choice of printing material and the calibration status of your 3D printer are foundational pillars for successfully printing complex geometries. Different materials possess unique properties that affect printability, detail reproduction, and post-processing capabilities. Likewise, a well-calibrated printer ensures dimensional accuracy, reliable performance, and consistent results, which are non-negotiable when dealing with intricate designs. Understanding these elements allows you to select the right tool for the job and ensure your printer is performing at its peak, ready to tackle the challenges posed by detailed STL files of cars and other complex objects.
The material you use directly impacts the outcome of your print:
For most hobbyist applications and detailed car models, PLA on FDM printers or standard resins on resin printers offer the best balance of detail, ease of printing, and cost.
A calibrated printer is essential for accurate and reliable printing. Neglecting calibration leads to dimensional inaccuracies, poor surface finish, and print failures.
Regular maintenance and periodic calibration checks are vital. This ensures that your printer is consistently performing at its best, ready to produce high-quality prints from even the most complex STL files.
Once your complex 3D print successfully emerges from the printer, the journey isn’t necessarily over. Post-processing is a critical step in achieving a professional, polished look, especially for detailed car models. This phase involves removing supports, cleaning up imperfections, and preparing the model for painting or final assembly. The techniques you employ here can significantly enhance the perceived quality of your print, masking any minor flaws and bringing out the intricate details of the design. Mastering these steps transforms a raw 3D print into a display-worthy piece.
Removing support structures is often the most delicate part of post-processing.
Achieving a smooth, paint-ready surface requires patience and technique.
With the model cleaned, filled, and primed, it’s ready for its final aesthetic treatment.
Taking the time for thorough post-processing elevates your 3D printed car models from hobbyist projects to impressive display pieces.
Even with meticulous preparation, 3D printing complex geometries can present unique challenges and lead to specific types of failures. Understanding these common pitfalls and their solutions is crucial for any maker aiming for consistent, high-quality results. Whether it’s sagging overhangs, detached prints, or clogged nozzles, knowing how to diagnose and fix the problem quickly can save time, material, and frustration. This section focuses on the most prevalent issues encountered when printing intricate models, such as those found on platforms like 88cars3d.com, and provides actionable advice for overcoming them.
This is perhaps the most common issue with complex geometries.
A print lifting off the build plate is a catastrophic failure.
Fine strings of filament or small blobs marring the surface.
Layers are misaligned, often appearing as a sudden jump.
Conclusion
Printing complex geometries, especially the detailed car models found on 88cars3d.com, requires a blend of technical understanding, careful preparation, and patient execution. By mastering the nuances of the STL file format, employing advanced slicing techniques, strategically generating and removing support structures, optimizing print orientation, selecting the appropriate materials, and ensuring your 3D printer is well-calibrated, you can significantly reduce the likelihood of print failures. Each step, from initial mesh repair to final post-processing, plays a vital role in transforming a digital design into a tangible masterpiece. Don’t be discouraged by initial setbacks; view them as learning opportunities. With practice and by applying the principles outlined in this guide, you’ll gain the confidence to tackle even the most challenging prints, bringing your passion for automobiles and 3D printing together in stunning detail. Happy printing!
“`
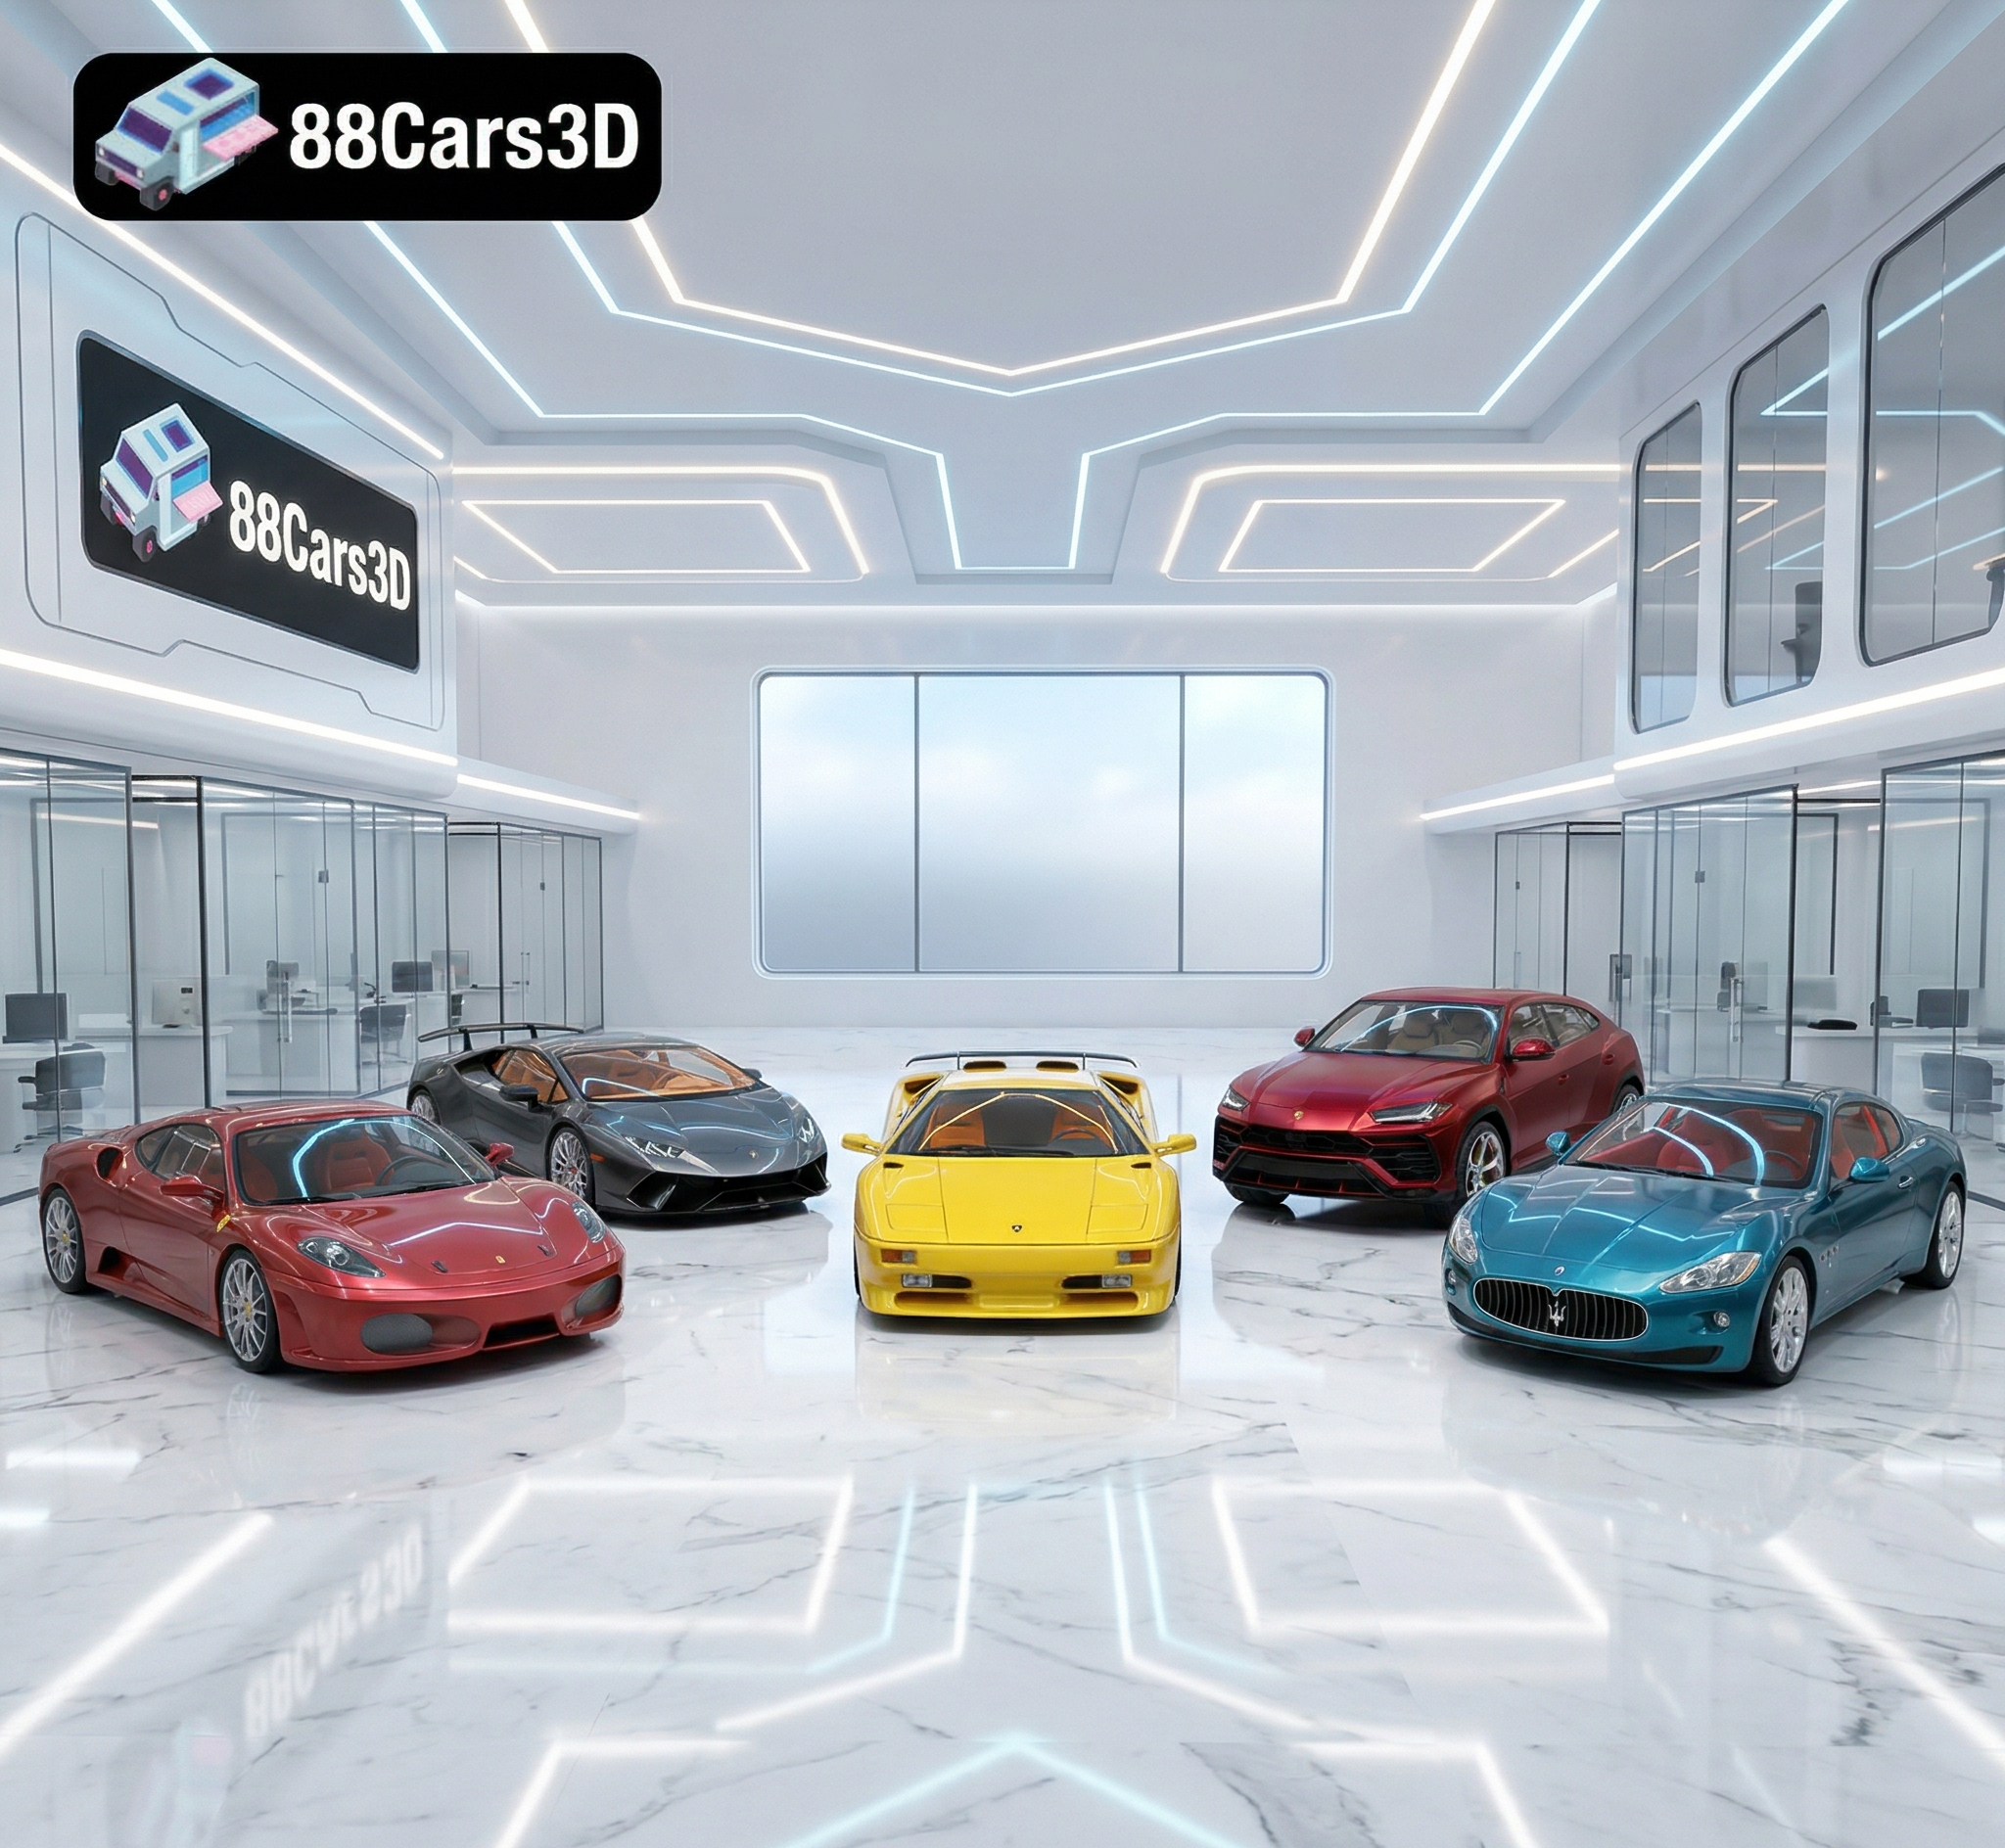
Texture: Yes | Material: Yes | 3D Printable: Yes. Download the Italian Thoroughbreds Bundle featuring 5 iconic 3D models: Lamborghini Huracán Performante, Ferrari 458 Italia, Lamborghini Urus, Diablo SV, and Maserati GT. Optimized for 4K rendering and 3D printing (STL included). Save 50% with this ultimate Italian vehicle collection.
Price: $199.99

Download the Elite Future Mobility Bundle featuring 4 highly optimized 3D models: Tesla Model S, Avatr 11, Li L9, and Zoox Robotaxi. Perfect for ArchViz, Smart City renders, and game dev. Optimized for Unreal Engine and Blender. Includes .fbx, .obj, and .max formats.
Price: $99
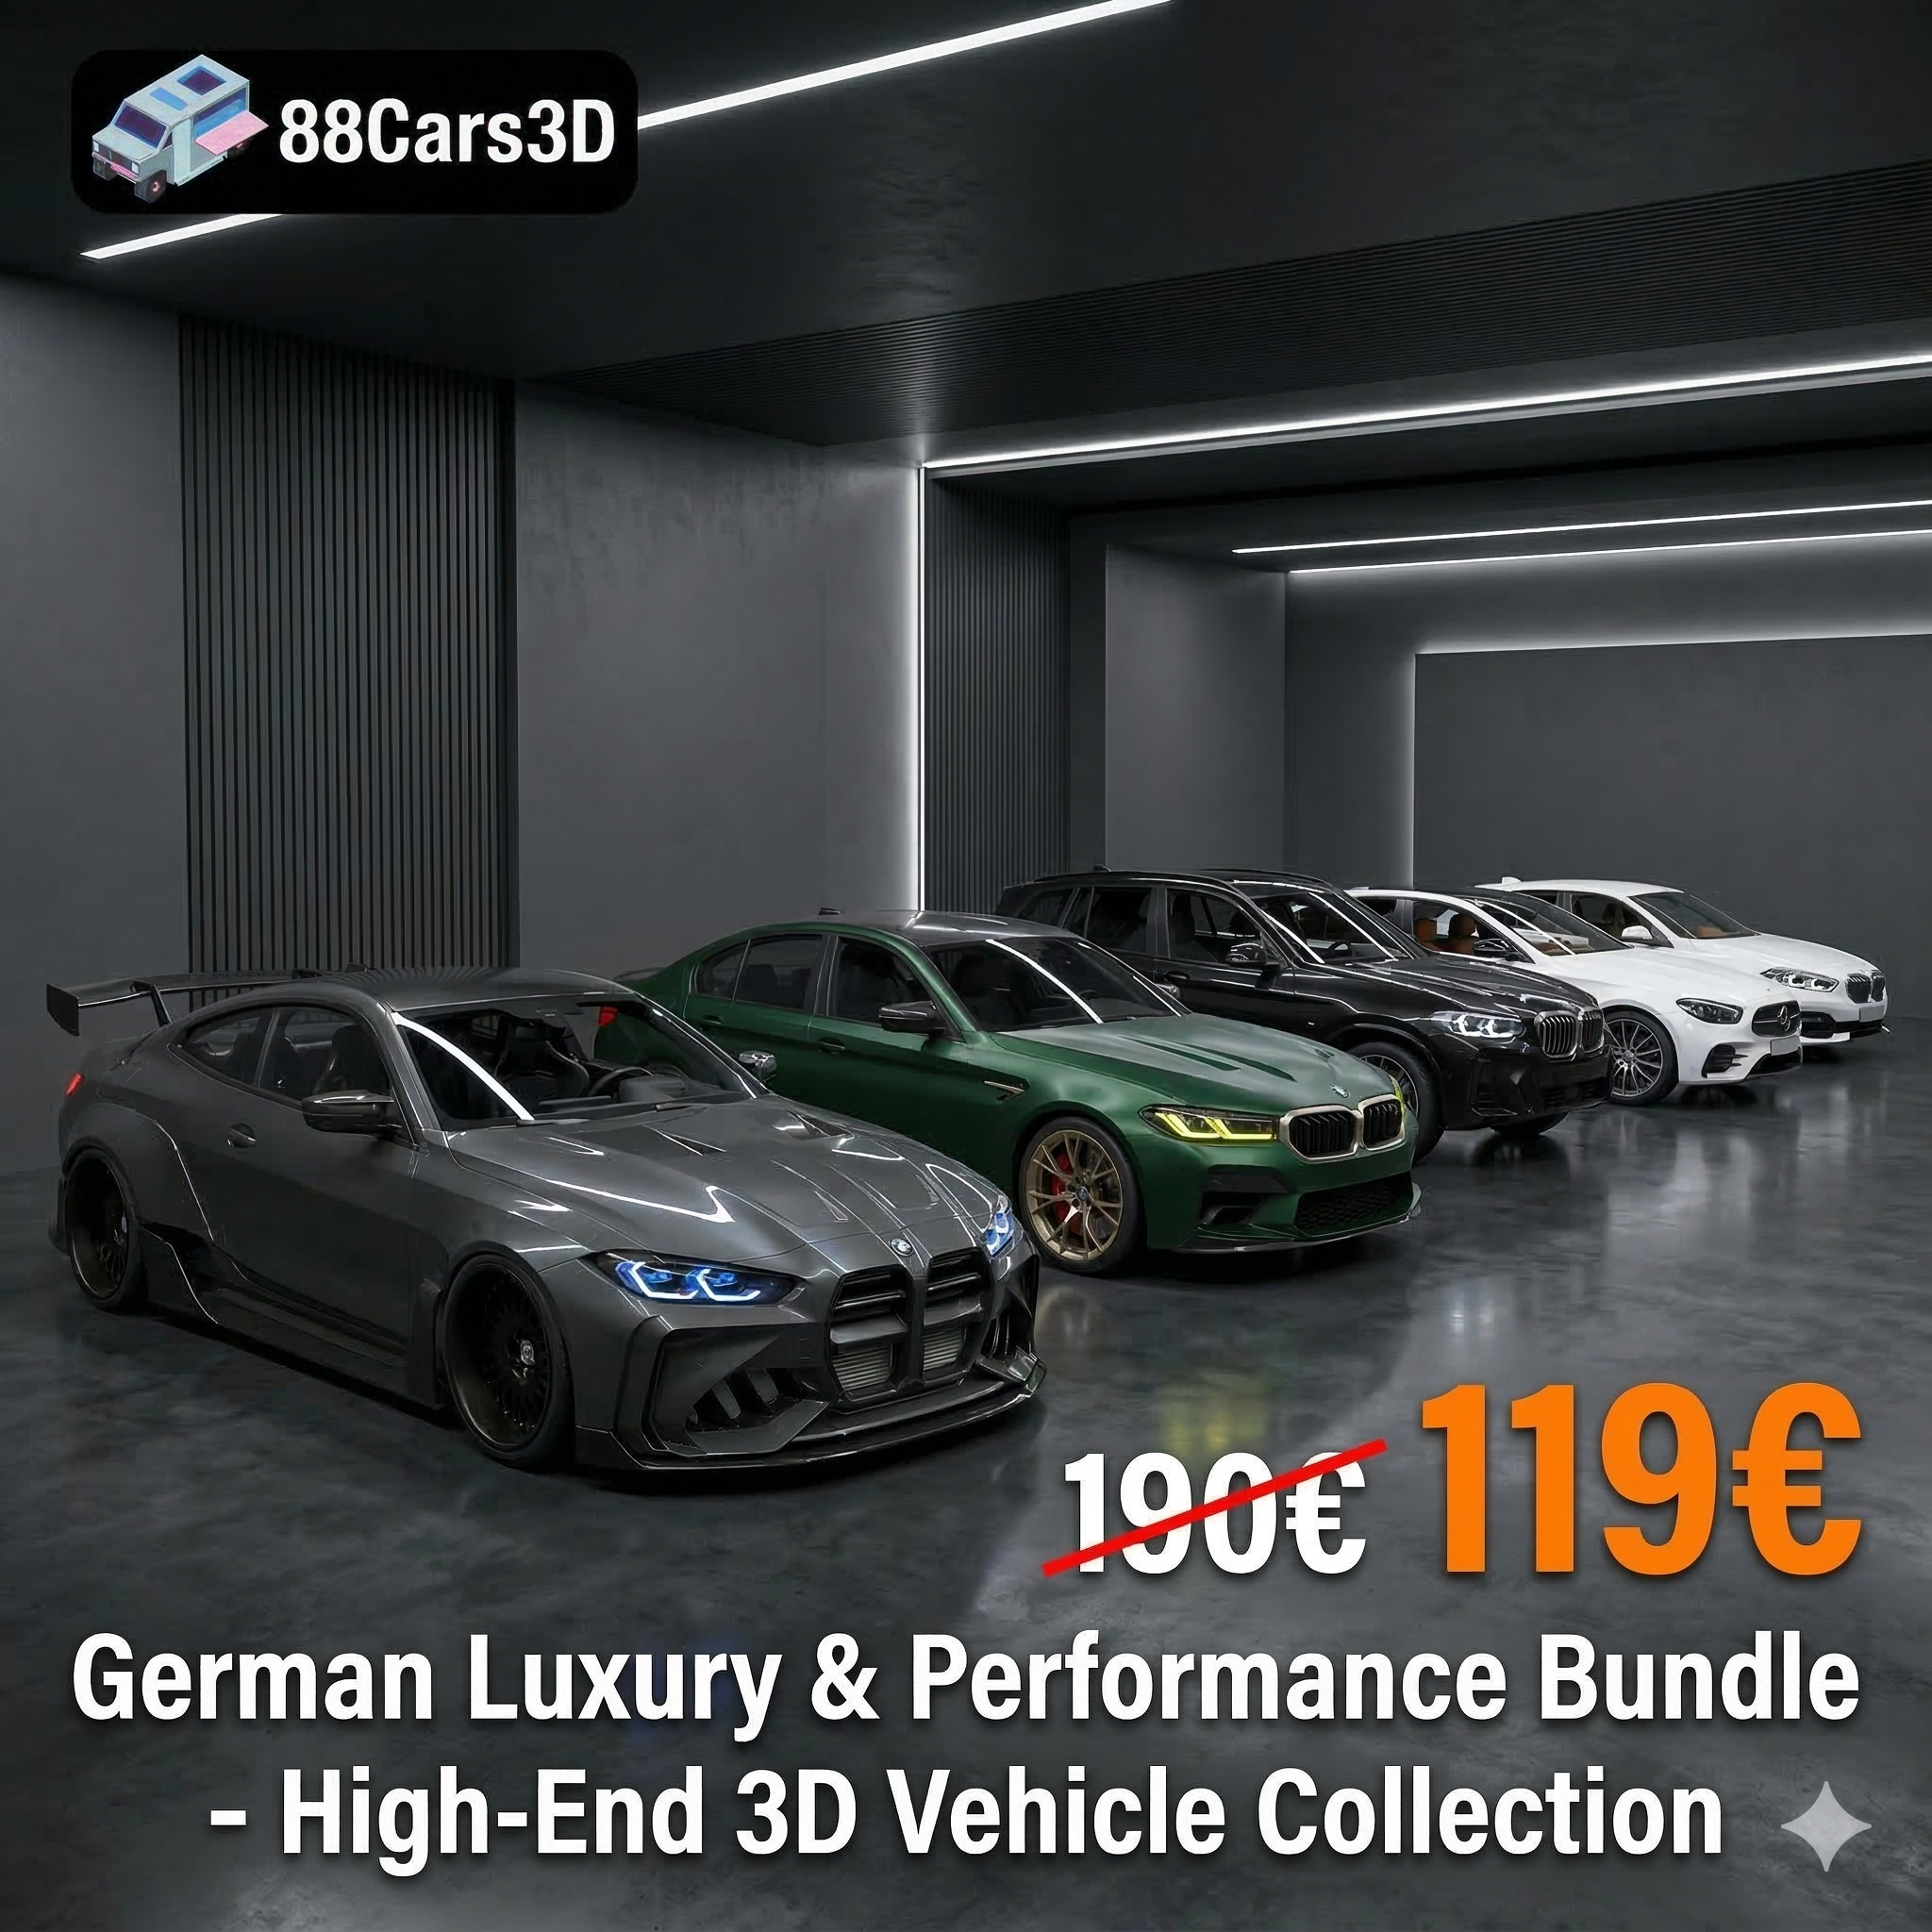
🚗 5 Iconic German Cars (BMW M4 G82, M5 CS, X3, 1 Series & Mercedes E-Class). ✅ Optimized for ArchViz: Ready for Corona & V-Ray. 💰 Save €71 with this limited-time collection! 🚀 Instant Download after purchase.
Price: $119
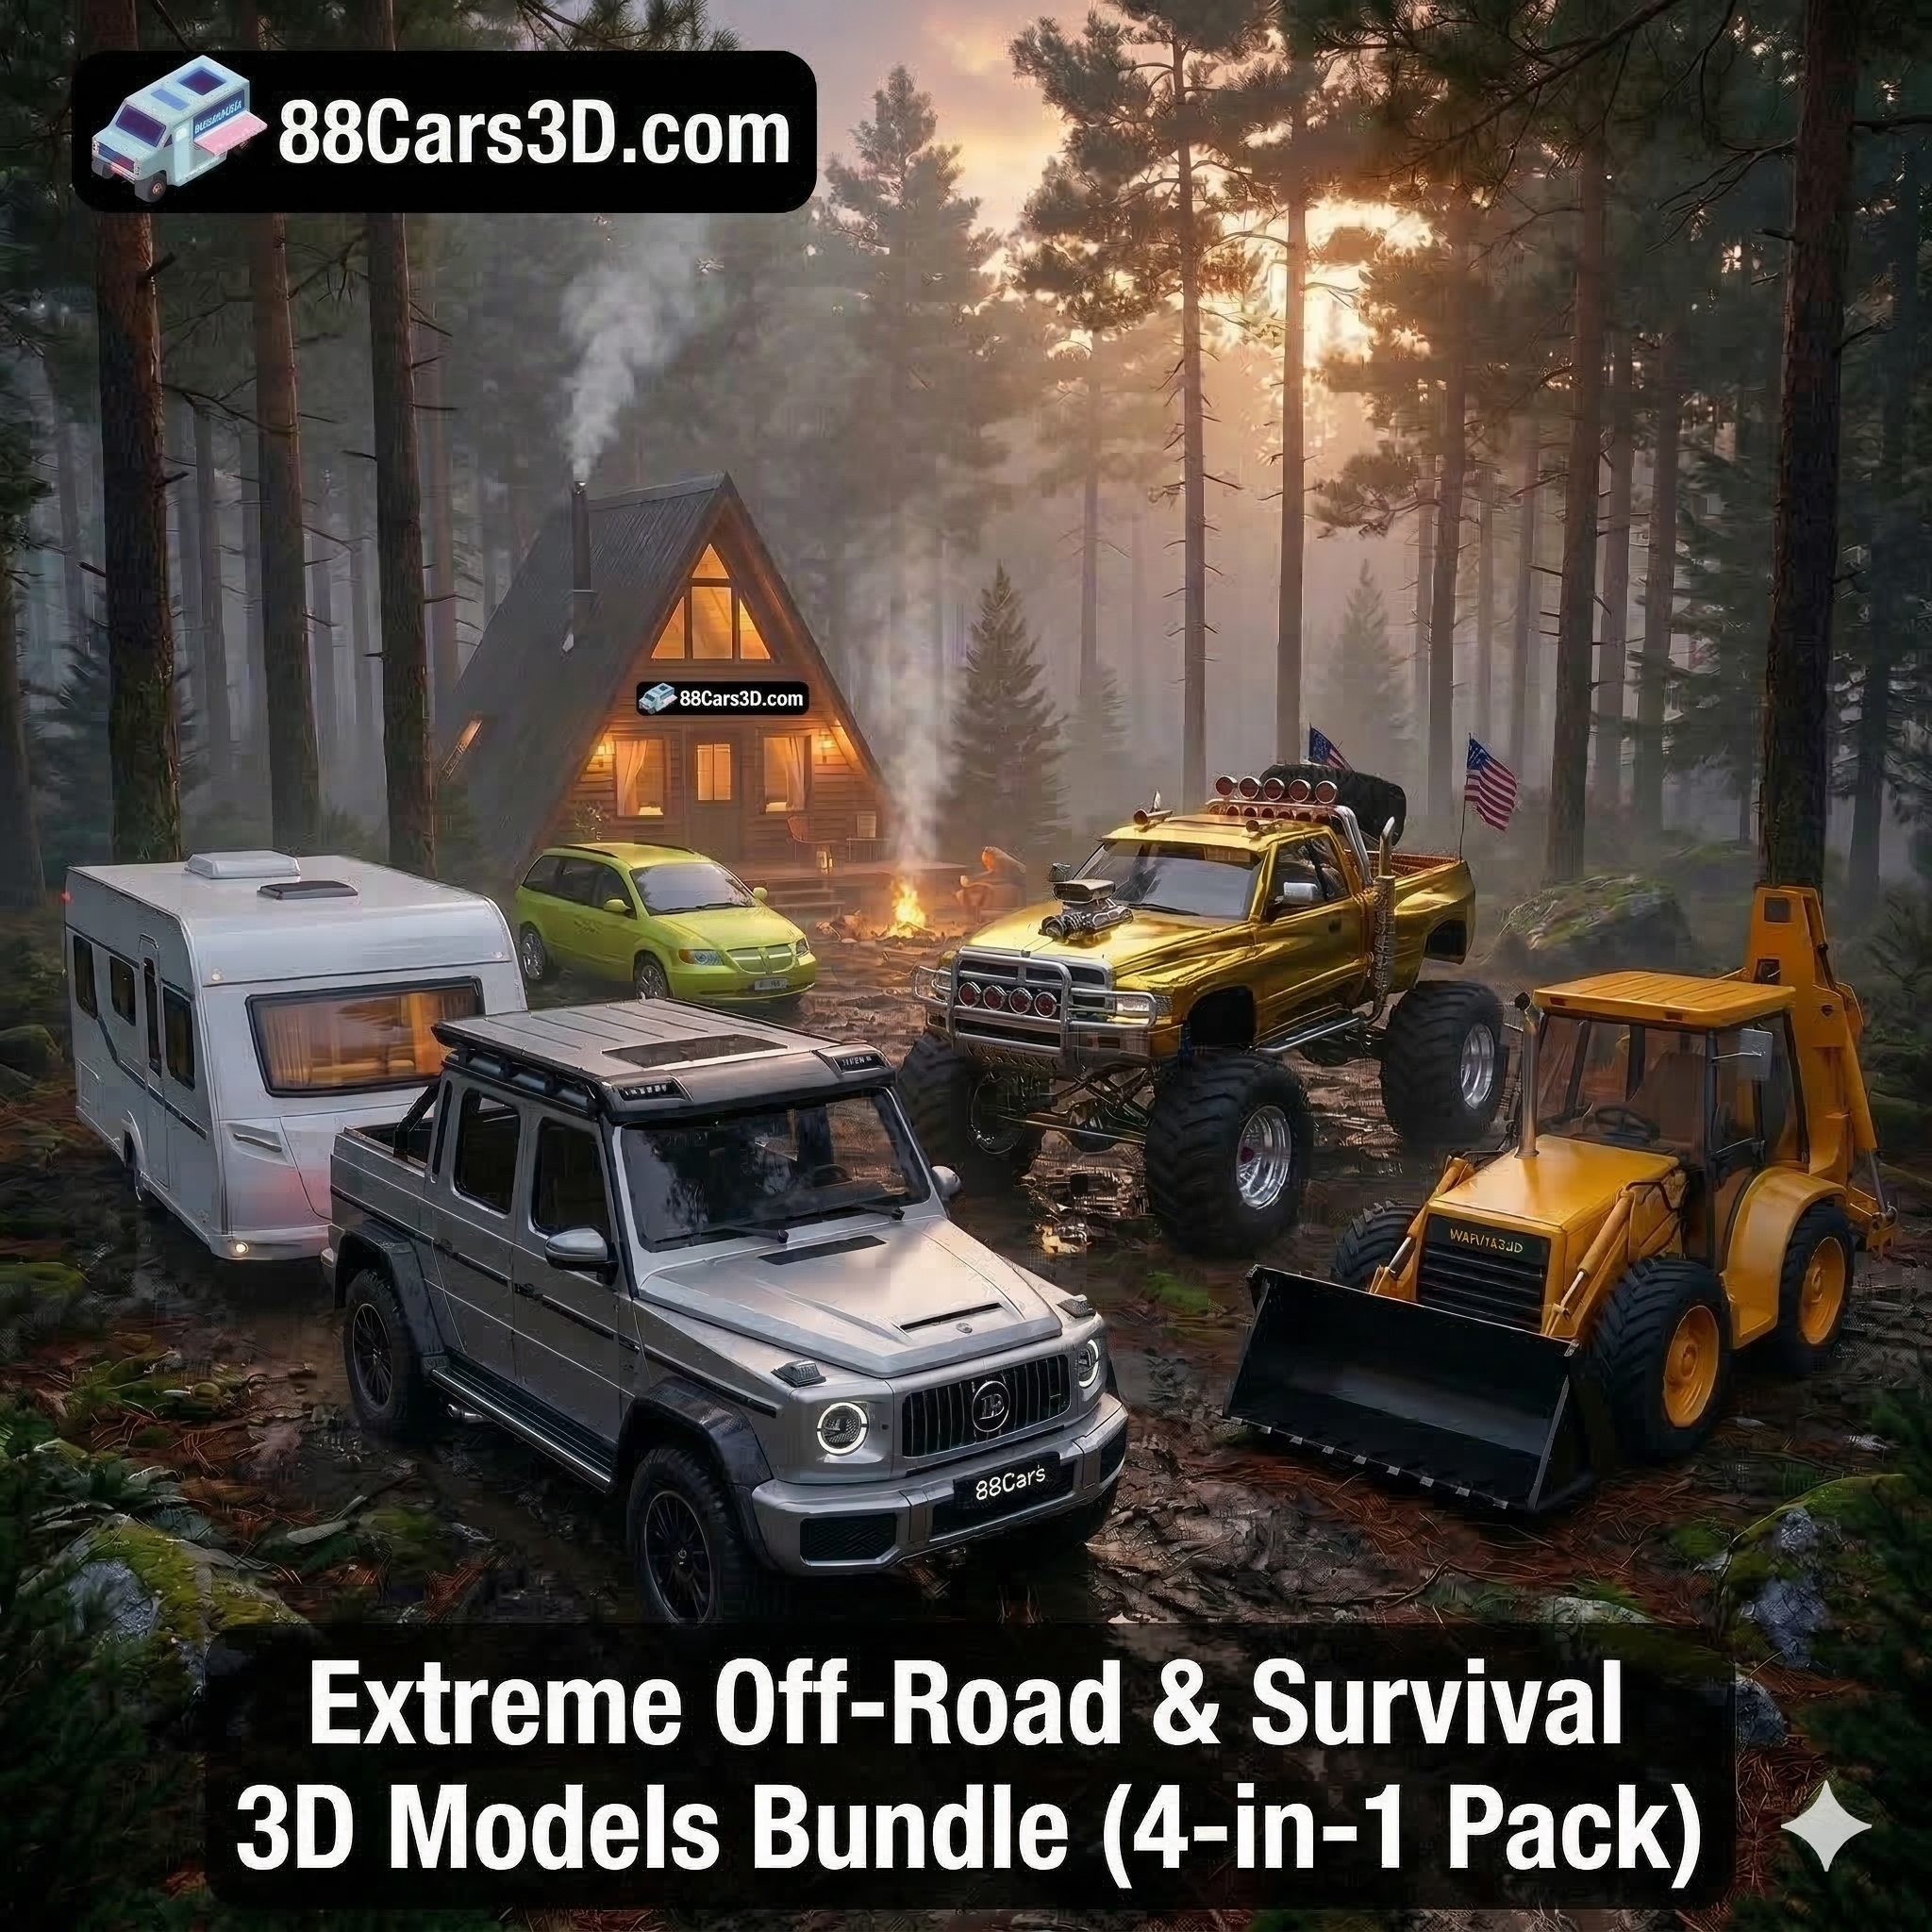
Download the Extreme Off-Road & Survival 3D Models Bundle! Includes the Brabus 800 Adventure, Dodge Ram Bigfoot, Spec Truck, and a Caravan. Save over €210 on this premium 4-in-1 off-grid vehicle pack for ArchViz and game development.
Price: $149.99
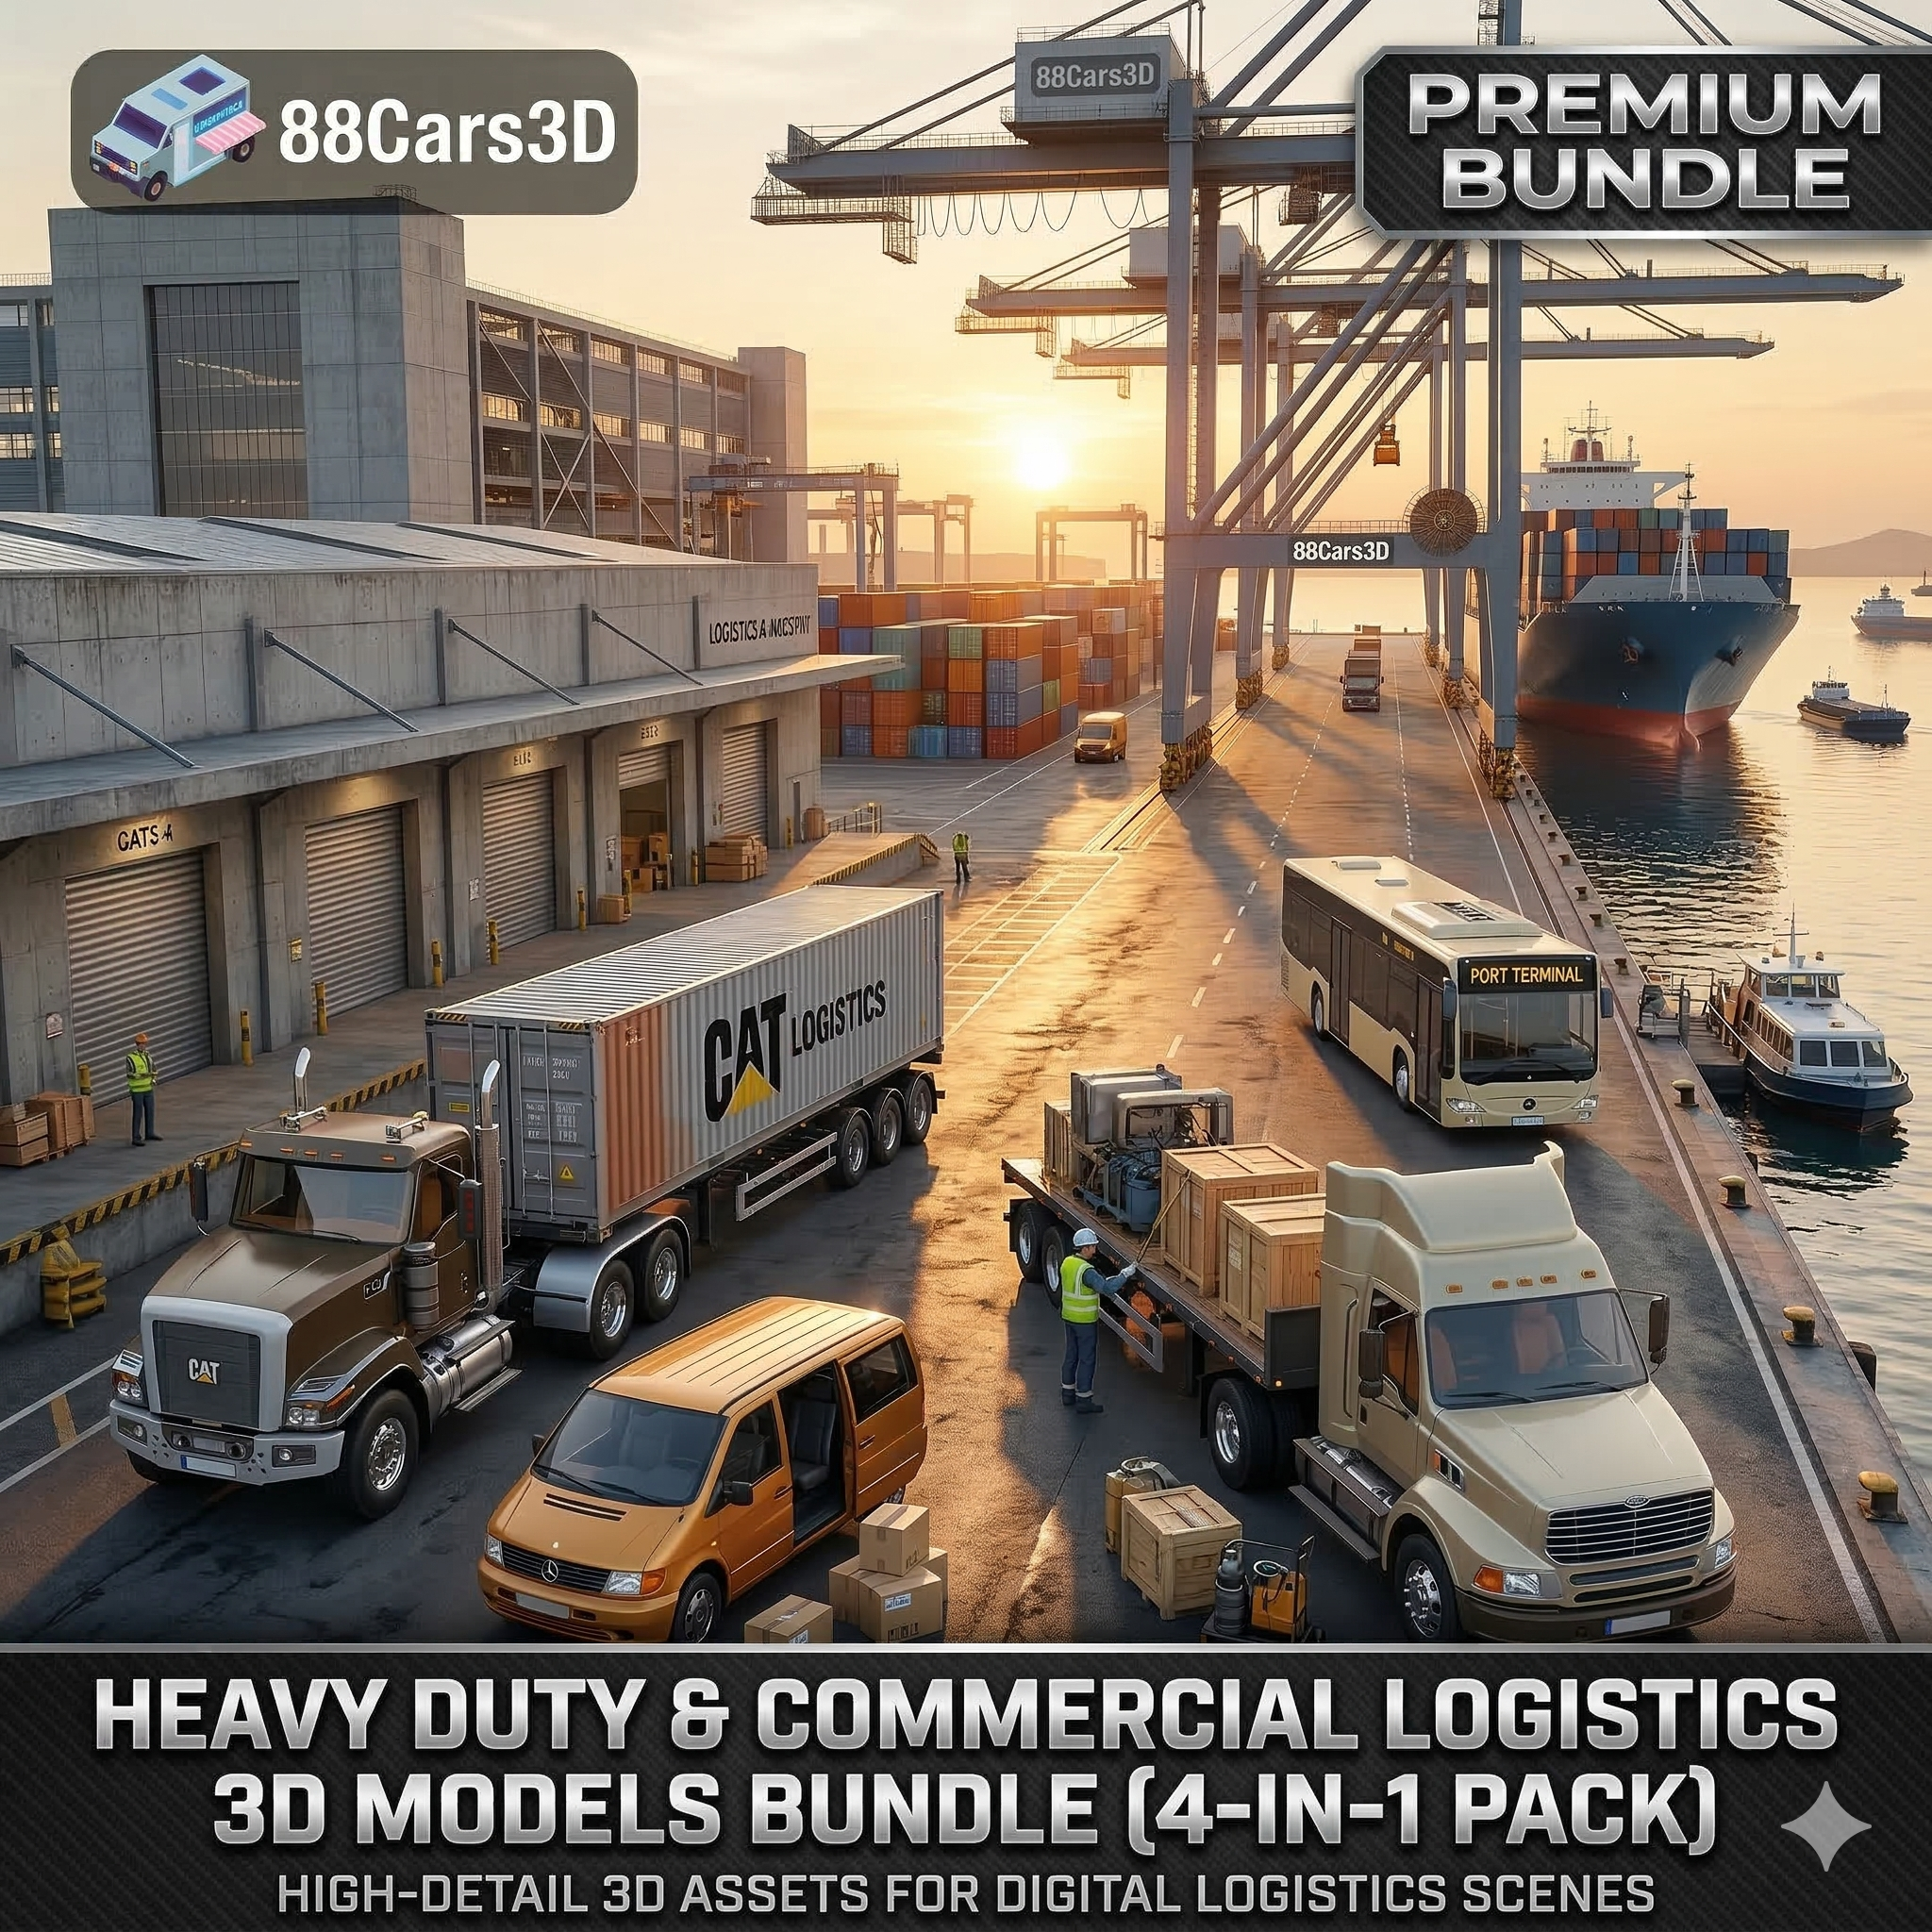
Download the Heavy Duty & Commercial Logistics 3D Models Bundle! Includes the Ford Sterling, Caterpillar CT680, Mercedes Citaro Bus, and Vito Van. Save over €130 on this massive, game-ready 4-in-1 industrial vehicle pack.
Price: $109.99

Download the Ultimate Custom Motorcycles 3D Models Bundle. Includes a Custom Chopper, Ducati 916 Café Fighter, Harley XR1200X, and BMW K100. Perfect premium props for luxury ArchViz garages. Save over €250 today!
Price: $159.99

Download the ultimate JDM Street Racing 3D Models Bundle! Includes the Nissan GT-R, Toyota Supra, Mazda RX-7, Lancer Evo IX, and Honda NSX. Save big on this highly optimized, game-ready 5-in-1 Japanese legend car pack.
Price: $129.99

Download the ultimate American Muscle & Cinematic Classics 3D Models Bundle! Includes the Dodge Charger ’68, Mustang Eleanor GT500, Camaro Z28 ’79, and a custom ’69 Mustang. Save over €240 on this game-ready, premium 4-in-1 pack.
Price: $149.99
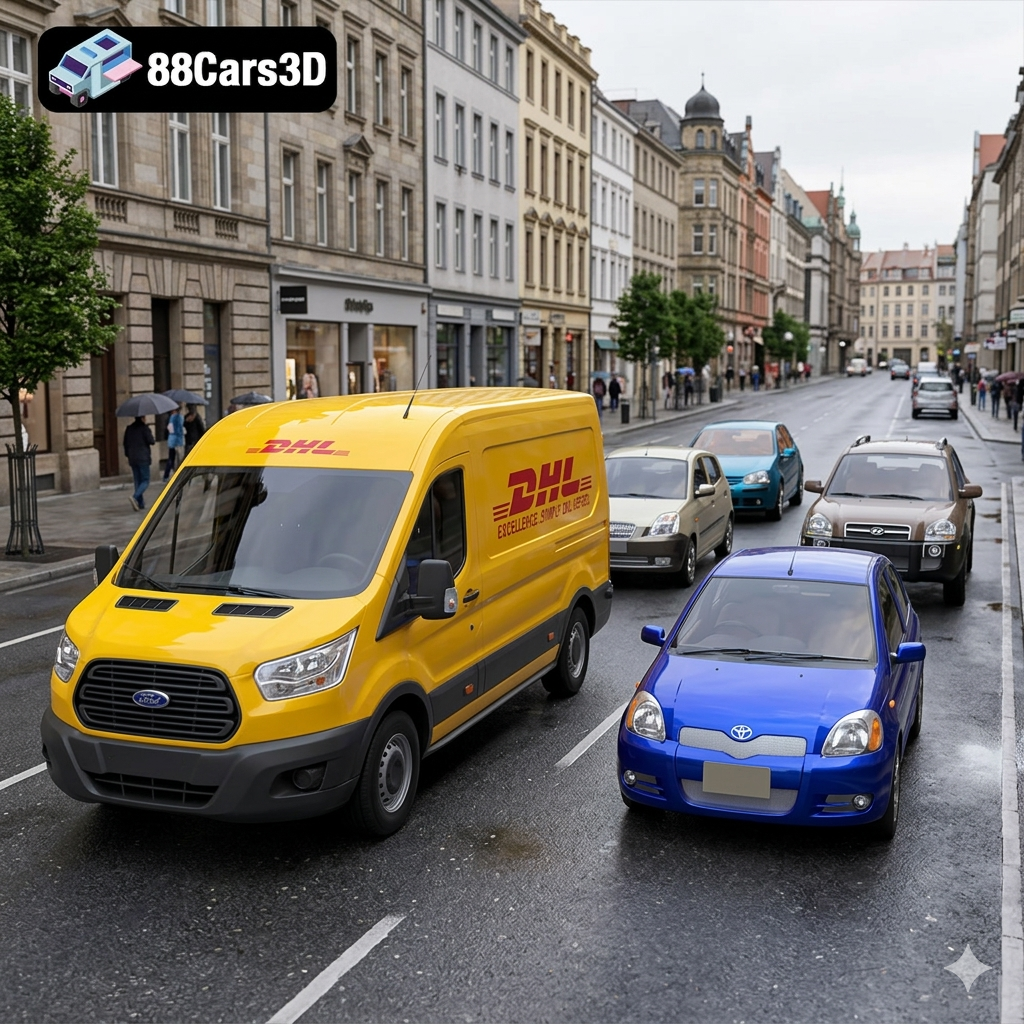
Download the Everyday City Traffic 3D Models Bundle. Includes the VW Golf, Kia Picanto, Hyundai Tucson, Toyota Yaris, and a DHL Ford Transit Van. Save big on this 5-in-1 pack, perfectly optimized for realistic ArchViz streets and game traffic.
Price: $99.99
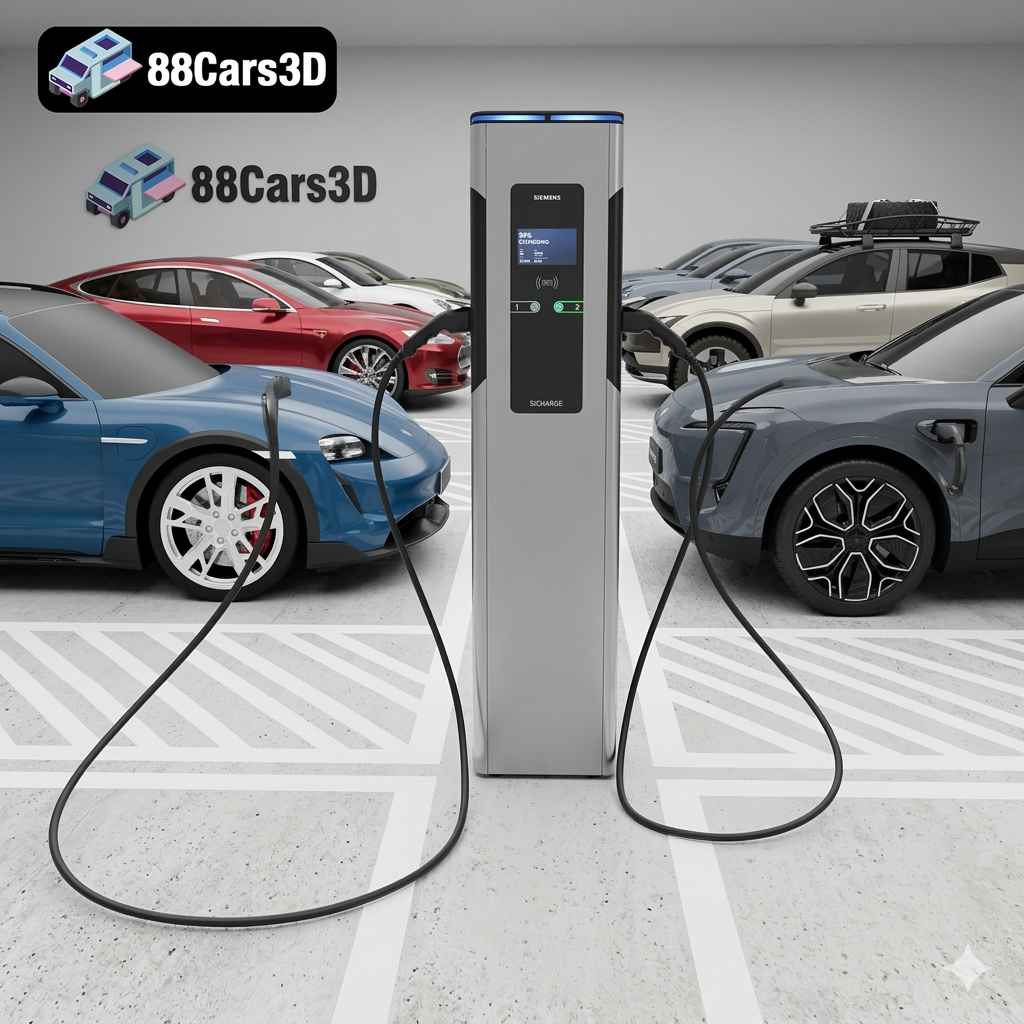
Download the Future of Mobility EV 3D Models Bundle. Includes the Volvo EX30, Tesla Model S, AVATR 11, Porsche Taycan, and a Siemens EV Charger. Save big on this highly optimized 5-in-1 pack for ArchViz and game development!
Price: $89.99

