Get 50% OFF All Premium 3D & STL Models!
“`html
The allure of bringing a meticulously crafted 3D printable car model to life on your desktop printer is undeniable. Whether you’re a seasoned maker looking to expand your collection with detailed replicas from platforms like 88cars3d.com, an automotive enthusiast craving a tangible representation of your favorite vehicle, or an educator seeking engaging learning tools, the journey from a digital STL file to a physical print is filled with exciting possibilities. However, achieving high-quality, fast prints requires more than just hitting the ‘print’ button. It involves a deep understanding of STL file preparation, slicing techniques, and printer optimization. This comprehensive guide will delve into the crucial aspects of scaling, hollowing, and optimizing your 3D models to dramatically improve print speed without sacrificing the exquisite detail that makes models from sources like 88cars3d.com so appealing. We’ll explore the intricacies of STL file structures, master slicing parameters, conquer support generation, and unlock advanced techniques to ensure your prints are not only faster but also more robust and visually stunning.
Before we can effectively manipulate and optimize STL files, it’s essential to grasp their fundamental structure. The Stereolithography (STL) file format is the de facto standard for 3D printing, representing a 3D object as a collection of interconnected triangles. Each triangle is defined by three vertices and a normal vector, indicating the outward-facing direction. This seemingly simple representation is powerful, but it also introduces nuances that can impact printability and optimization.
The arrangement and connectivity of these triangles, known as mesh topology, are critical. A “watertight” or “manifold” mesh is one where there are no holes, gaps, or self-intersecting surfaces, ensuring the printer can interpret a closed volume to fill and print. Non-manifold meshes, often resulting from modeling errors or improper exporting, can lead to slicing failures, print artifacts, and unexpected outcomes. Understanding how your slicing software interprets this mesh topology is the first step in troubleshooting common printing issues and preparing your models for success.
Downloadable models, especially complex ones like detailed car replicas, can sometimes suffer from mesh errors. Common issues include:
Fortunately, specialized software can address these issues. Tools like Meshmixer (free), Blender (free), and Netfabb (paid) offer robust mesh repair capabilities. Using their automated repair functions or manually adjusting vertices and faces can fix most problems, ensuring your STL file is clean and ready for slicing. For instance, Meshmixer’s ‘Make Manifold’ feature is often a lifesaver for problematic meshes.
Scaling is perhaps the most straightforward yet impactful optimization technique. It allows you to adjust the size of a model to fit your build volume, meet specific display requirements, or improve print time by reducing overall material usage and complexity.
Most slicing software, including Cura, PrusaSlicer, and Simplify3D, provides intuitive scaling tools. You can typically adjust the X, Y, and Z dimensions independently or uniformly. For most car models, maintaining the aspect ratio (uniform scaling) is crucial to preserve the vehicle’s proportions. However, sometimes you might need to scale specific axes to fit your printer’s build plate or to compensate for shrinkage of certain materials.
When scaling models from marketplaces like 88cars3d.com, keep these points in mind:
For FDM printers with a 0.4mm nozzle, a minimum wall thickness of 0.8mm to 1.2mm is generally recommended for structural integrity and detail visibility. Resin printers, with their higher resolution, can often resolve much finer details and thinner walls.
The relationship between scaling and print time is linear. Doubling the dimensions of a model (scaling by 200%) will increase its volume by a factor of eight (23), significantly extending print time and material consumption. Conversely, reducing a model by half (50%) will decrease print time and material by approximately eight times. This makes scaling a powerful tool for rapid prototyping or creating smaller, faster-to-print display pieces.
For larger models, especially those intended for display rather than structural testing, printing them solid can be incredibly time-consuming and wasteful of filament or resin. Hollowing is the process of removing the internal volume of a model, leaving only a thin outer shell. This dramatically reduces print time, material usage, and weight.
Modern slicers offer built-in hollowing features. In Cura, for example, you can enable ‘Hollow’ under the Shell settings, specifying a wall thickness. PrusaSlicer has a similar ‘Hollow’ option. When these features are enabled, the slicer intelligently carves out the interior, leaving the specified wall thickness. However, it’s crucial to understand that this internal hollowing usually doesn’t create an opening for material to escape or for support structures to be removed. This leads to the concept of ‘drain holes’.
For resin printing (SLA/DLP/MSLA), hollowing is almost always essential for larger models. Without drain holes, uncured resin can get trapped inside, leading to potential leaks, print failures, and safety hazards. Drain holes, typically 2-3mm in diameter, should be strategically placed on the lowest, least visible surfaces of the model. Slicers can often automatically add these, or you can create them manually using 3D modeling software like Meshmixer or Blender. Ensure your slicer is set to ‘Hollow’ and specify a wall thickness (e.g., 1.5-3mm for resin models) and add drain holes. The slicer will then print the hollowed object with the specified walls and holes.
Sometimes, automatic hollowing might not produce the desired results, especially with models featuring complex internal geometry or if you need precise control over the hollowing process. In such cases, manual hollowing in 3D modeling software is the way to go.
This method gives you complete control over the thickness of the walls and the placement of any necessary openings.
Once your model is scaled and potentially hollowed, the next frontier is optimizing your slicer settings. This is where the magic happens, balancing speed with print quality and ensuring successful completion.
The layer height directly impacts how much detail your printer can resolve and, crucially, how long a print takes. A smaller layer height (e.g., 0.1mm) results in finer details and smoother curves but significantly increases print time because the printer has to lay down many more layers. Conversely, a larger layer height (e.g., 0.2mm, 0.3mm) prints much faster but with a more noticeable layer texture. For car models where smooth body panels are desirable, finding the sweet spot is key. For FDM printing, 0.2mm is often a good compromise. For internal components or parts where detail isn’t paramount, 0.28mm or 0.3mm can drastically reduce print times.
Slicers provide numerous speed settings. While increasing overall print speed can seem like the obvious solution, it’s more nuanced.
Experimenting with these individual speeds is more effective than a blanket increase. For example, printing inner walls and infill at 80 mm/s while keeping the outer walls at 40 mm/s can nearly halve the print time for the bulk of the model.
Infill provides internal support for the outer walls and top layers. High infill density (e.g., 100%) is unnecessary for display models and dramatically increases print time and material usage. For most decorative prints, an infill density of 5-15% is sufficient. Patterns also play a role.
For speed optimization on display models, a low-density (5-10%) grid or lines pattern is often the best choice. If the model needs to be more robust, consider a slightly higher density (15-20%) with a gyroid pattern.
Beyond basic slicing, strategic decisions about model orientation, support structures, and bed adhesion can significantly influence print success, speed, and post-processing effort.
The way you orient your model on the build plate is critical.
For car models, printing the main body upright or slightly tilted often works well. Wheels and smaller components might print best laid flat.
Supports are often necessary for bridging and overhangs. Modern slicers offer various support types and settings:
When removing supports, use appropriate tools like pliers, flush cutters, and hobby knives carefully. For FDM prints, a slight ‘over-extrusion’ on the support interface can make them easier to break away cleanly. For resin prints, supports are often delicate and require careful cutting and sanding.
A print failing due to poor bed adhesion is a time and material killer.
For most car models, a brim is usually sufficient. Ensure your build plate is clean (IPA is your friend!) and leveled correctly. Using adhesives like glue stick or hairspray can also enhance adhesion for materials prone to warping, like ABS.
Even with perfect slicing, the wrong material or an uncalibrated printer can sabotage your efforts.
Different materials offer different properties, influencing print speed, quality, and post-processing.
For speed, standard resins and PLA are generally the quickest to print if set up correctly, provided your printer can handle the necessary speeds without compromising quality.
A well-calibrated printer is fundamental for consistent, high-quality prints. Key calibration steps include:
Regularly performing these calibrations, especially after changing nozzle sizes or materials, will save you countless hours of troubleshooting and failed prints. If you’re using a new nozzle size, remember to adjust your line width settings in the slicer accordingly.
Bringing digital 3D printable car models to life is a rewarding endeavor, and by mastering the art of scaling, hollowing, and optimization, you can significantly enhance both the speed and quality of your prints. We’ve explored the importance of understanding STL file structures and the necessity of mesh repair. We’ve seen how strategic scaling can adapt models to your needs while mindful hollowing, especially with drain holes for resin printing, dramatically reduces material and time. Crucially, we’ve dived deep into slicing parameters – layer height, individual print speeds, infill patterns, and densities – all vital for shaving off precious hours. Furthermore, the intelligent use of print orientation, advanced support strategies, and robust bed adhesion techniques lay the groundwork for successful, frustration-free printing. Finally, remembering that material choice and consistent printer calibration are the bedrock upon which all these optimizations stand, ensures you’re set up for success.
By applying these principles consistently, you’ll find yourself printing stunning replicas from sites like 88cars3d.com more efficiently than ever before. Don’t be afraid to experiment; tweak settings, test different orientations, and observe the results. Each print is a learning opportunity. Start with models that are already well-prepared, such as those found on specialized marketplaces, and gradually apply these advanced techniques. The journey from a digital file to a perfectly printed model is one of continuous learning and refinement. Embrace the process, and enjoy the incredible automotive creations you’ll build!
“`
Texture: Yes
Material: Yes
Download the Toyota MRS-007 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Porsche 911 Turbo S 2024 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $20

Texture: Yes
Material: Yes
Download the Pontiac Solstice 2009 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Mini Cooper Countryman 2025 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $29.9
Texture: Yes
Material: Yes
Download the Mercedes C Classe 2012 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $19.9
Texture: Yes
Material: Yes
Download the Mercedes-Benz S65 AMG 2018 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $19.9
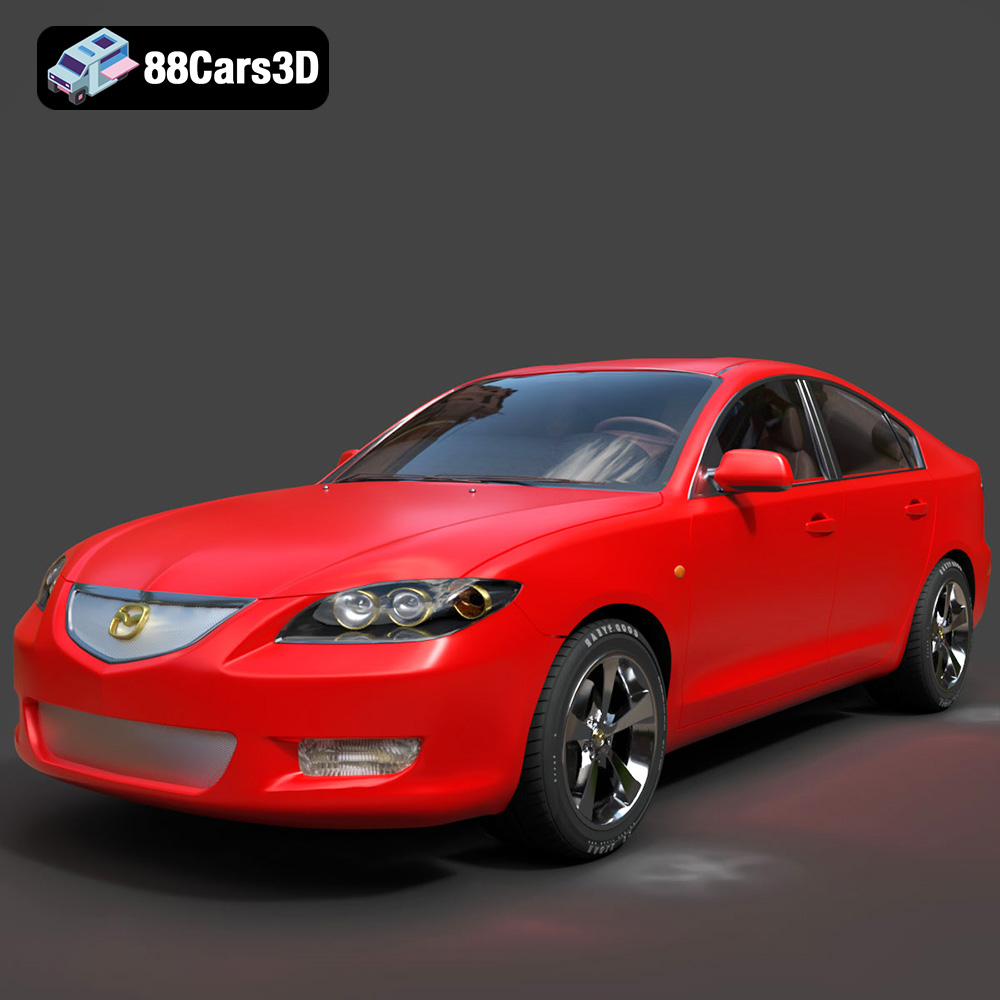
Texture: Yes
Material: Yes
Download the Mazda 3 Sedan 2004 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10

Texture: Yes
Material: Yes
Download the Martin Rapide 2011 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $20.9
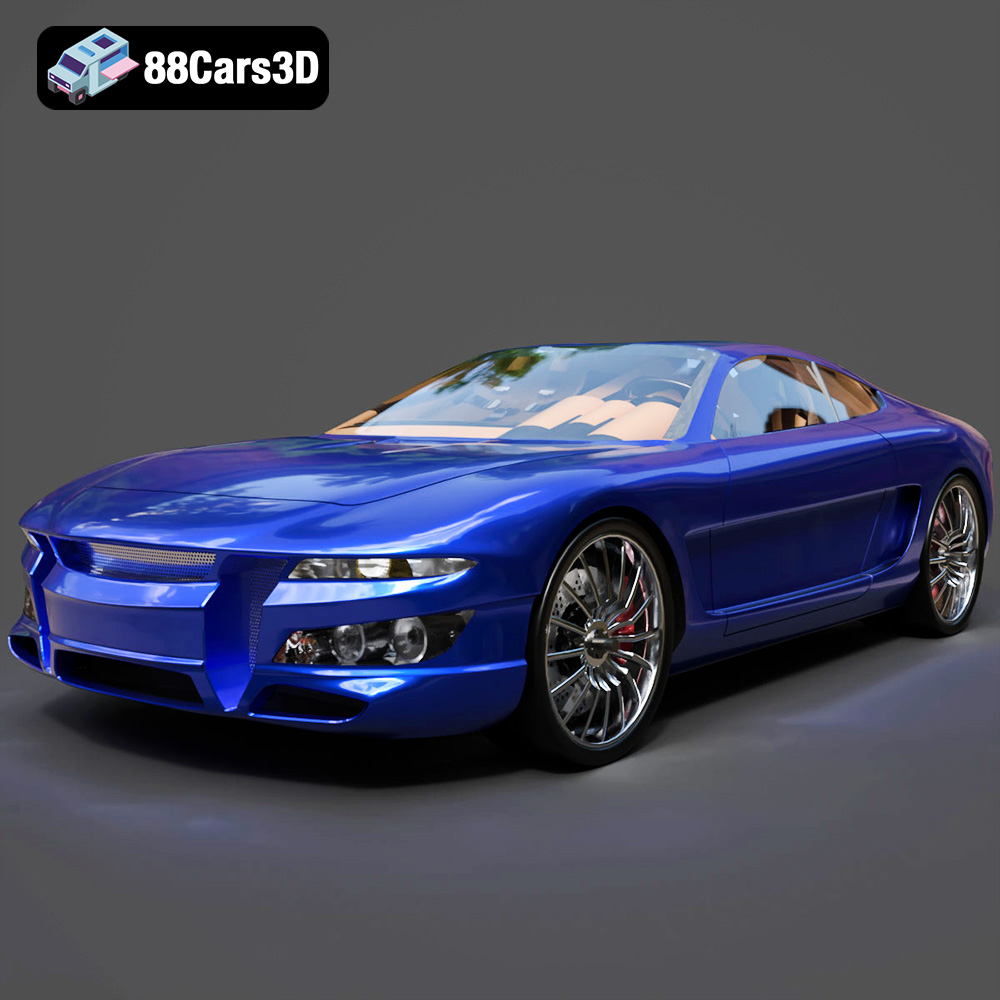
Texture: Yes
Material: Yes
Download the Car Tasergal 005 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $10
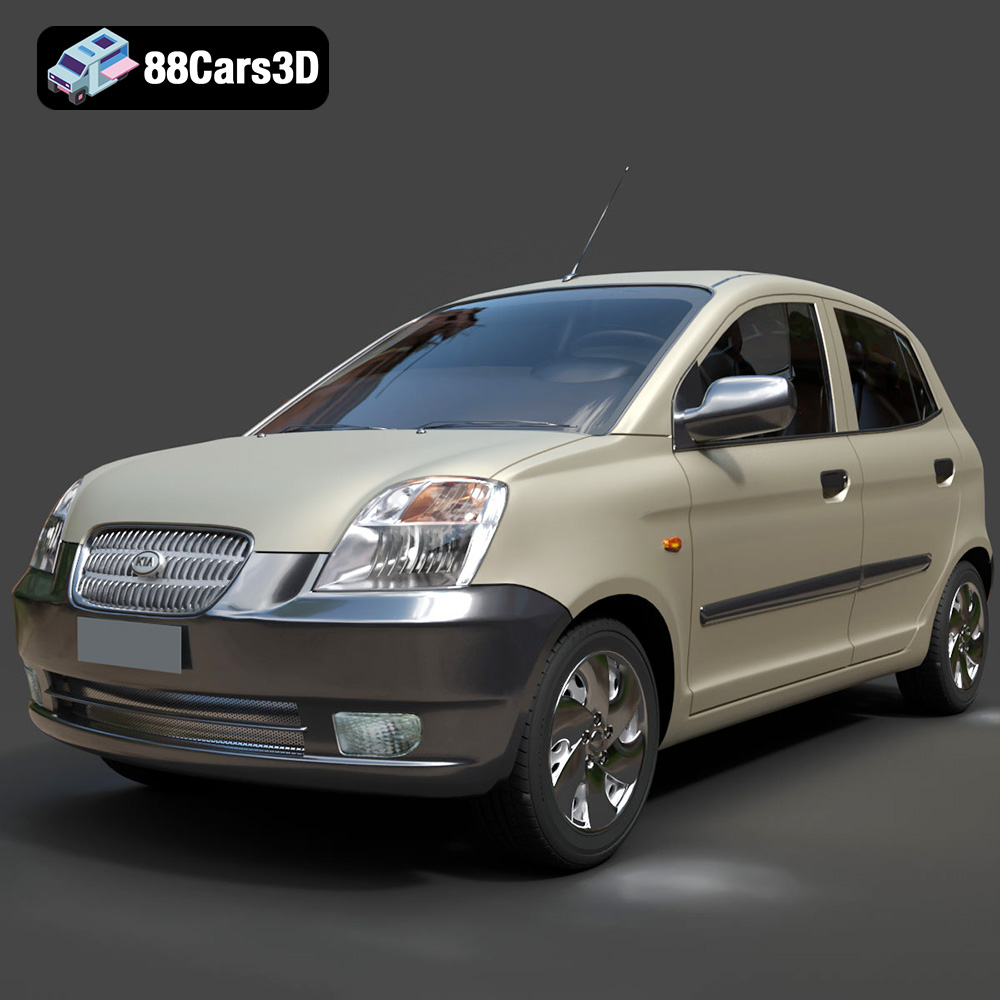
Texture: Yes
Material: Yes
Download the Kia Picanto 2024 3D Model featuring clean geometry, realistic detailing, and a fully modeled interior. Includes .blend, .fbx, .obj, .glb, .stl, .ply, .unreal, and .max formats for rendering, simulation, and game development.
Price: $15.99

