
“`html
Mastering Your 3D Prints: Avoiding the Top 10 Pitfalls with STL Car Models
The allure of bringing meticulously designed 3D car models to life through additive manufacturing is undeniable. From classic muscle cars to futuristic concepts, the world of printable automotive STL files offers a vast playground for hobbyists and enthusiasts. However, the journey from a digital file to a flawless physical object is often paved with unexpected challenges. Many beginners, eager to start printing, stumble into common traps that can lead to failed prints, wasted materials, and frustrating setbacks. Understanding these pitfalls is the first step towards consistent, high-quality results. This comprehensive guide will delve into the ten most frequent mistakes beginners make when printing STL files, particularly focusing on detailed automotive models like those found on 88cars3d.com, and provide actionable strategies to overcome them. By mastering these techniques, you’ll significantly improve your printing success rate, save time and resources, and unlock the true potential of your 3D printer.
1. Neglecting File Preparation and Mesh Integrity
One of the most fundamental, yet often overlooked, steps in 3D printing is ensuring the integrity of the STL file itself. While many models from reputable sources like 88cars3d.com are designed to be print-ready with clean geometry, not all STL files are created equal. Issues like non-manifold geometry (where edges are shared by more than two faces), inverted normals (faces pointing inwards), holes in the mesh, or intersecting geometry can cause significant problems for slicing software. These errors can lead to distorted prints, missing sections, or even complete slicing failures. Beginners often assume an STL file will just “work” without verification, leading to immediate disappointment.
Understanding STL Structure and Common Errors
The STL format represents a 3D model’s surface geometry as a collection of triangular facets. Each facet is defined by three vertices and a normal vector indicating its outward direction. Errors arise when this structure is compromised. For instance, a hole in the mesh means the model isn’t “watertight,” preventing the slicer from calculating a solid volume. Inverted normals can confuse the slicer about which side of the surface is “inside” and “outside.” Intersecting triangles create ambiguous internal volumes.
Essential Mesh Repair Workflows
Before sending a file to your slicer, it’s crucial to inspect and repair it. Software like Meshmixer, Blender, or even built-in tools within some slicers (like PrusaSlicer’s mesh repair) can help. Common repair actions include:
- Detecting and Filling Holes: Automatically or manually closing gaps in the mesh.
- Recalculating Normals: Ensuring all faces are oriented correctly outwards.
- Simplifying or Decimating: Reducing the triangle count in overly complex meshes without significant loss of detail, which can improve slicing performance.
- Checking for Self-Intersections: Identifying and resolving areas where the mesh intersects itself.
For high-quality car models, especially those with intricate details like panel gaps or engine components, ensuring mesh integrity is paramount. Spending a few minutes checking a file can save hours of printing time and material.
2. Incorrect Slicing Parameters: The Balancing Act
The slicing software (e.g., Cura, PrusaSlicer, Simplify3D) is the bridge between your digital STL file and your 3D printer. It converts the model into a series of thin layers and generates the G-code instructions the printer follows. Beginners frequently use default settings or guess at parameters, leading to prints that are either too weak, too rough, or take an unnecessarily long time to print. Achieving a balance between print quality, speed, and structural integrity requires a deliberate approach to slicing.
Layer Height: Quality vs. Time
Layer height is perhaps the most significant setting affecting print quality and time. A smaller layer height (e.g., 0.1mm) results in finer details and smoother curves, ideal for the smooth bodywork of car models. However, it drastically increases print time. A larger layer height (e.g., 0.2mm or 0.3mm) prints much faster but leaves visible layer lines. For detailed car models, a layer height between 0.1mm and 0.15mm is often a good starting point, adjusting based on the specific printer and desired outcome. Finding this tradeoff is key; don’t settle for rough prints if detail is what you’re after.
Print Speed and Acceleration: The Sweet Spot
Printing too fast is a common mistake. While tempting to speed up prints, exceeding your printer’s capabilities can lead to ringing artifacts, poor layer adhesion, and failed prints. For detailed models, especially those with overhangs and fine features, reducing print speed (e.g., 40-60 mm/s for outer walls) is crucial. Similarly, acceleration and jerk settings influence how quickly the printer changes direction. High acceleration can cause vibrations and inaccuracies. Experimenting with these settings on calibration prints before tackling your car model is highly recommended.
Infill Density and Patterns: Strength and Material Usage
The infill is the internal support structure of your print. For decorative car models, high infill density (e.g., 20%+) is often unnecessary and wastes material and time. An infill density of 10-15% is usually sufficient for structural support and can be increased for parts that require more durability. Different infill patterns (e.g., grid, gyroid, cubic) offer varying levels of strength and printability. Gyroid is often favored for its strength in all directions and efficient material usage. Choosing the right infill can optimize both the model’s durability and your material consumption.
3. Inadequate or Improper Support Structures
Many 3D car models feature complex geometries with overhangs, bridges, and steep angles – elements that require support structures to print successfully. Beginners often underestimate the need for supports, try to print with minimal or no supports, or generate supports incorrectly. This inevitably leads to sagging, drooping, or completely failed overhangs and bridges, ruining the delicate details of the car’s body, spoiler, or undercarriage.
Identifying Areas Needing Support
Most slicing software can automatically generate supports, but it’s essential to understand *why* they are needed. Any part of the model that extends outwards at an angle greater than about 45-60 degrees from the vertical typically requires support. This includes spoilers, wheel arches, bumpers, mirrored surfaces, and even areas beneath the chassis. Reviewing the sliced model layer-by-layer in the slicer is crucial to identify all potential problem areas.
Support Settings: Type, Density, and Placement
Choosing the right support settings is vital for clean results and easy removal. Beginners often use default “normal” supports, which can be difficult to remove and leave significant marks. Consider these options:
- Tree Supports: These branch-like supports often use less material, are easier to remove, and can be positioned more precisely, making them excellent for detailed models.
- Support Density: Lowering support density (e.g., 10-15%) makes them easier to break away.
- Support Interface: Adding a support roof or interface layer can create a smoother surface where the support touches the model, reducing cleanup.
- Support Z Distance: Increasing the gap between the support and the model (e.g., 0.2mm or higher, depending on layer height) makes removal easier, but too large a gap can lead to drooping.
Manually tweaking support placement, adding “touching buildplate only” options, or even manually adding/removing supports in specialized software can greatly improve results, especially for complex models downloaded from marketplaces like 88cars3d.com.
4. Poor Print Orientation and Bed Adhesion
How you orient your 3D car model on the print bed and ensuring it sticks firmly are critical for a successful first layer and overall print stability. Beginners often just place the model flat on its underside without considering the implications for overhangs, support needs, or the first layer’s adhesion. A poorly adhered first layer can lead to prints detaching mid-print, resulting in a catastrophic failure.
Strategic Model Orientation
The orientation of your model can significantly impact print quality and the need for supports. For car models:
- Flat Underside: Placing the car model flat on its roof or underside (if it has a flat surface) can minimize the need for supports on the main body, but might create challenging overhangs for details like wheel wells or bumpers.
- On its Wheels: Printing a car on its wheels is often aesthetically pleasing for display, but typically requires extensive supports for the wheel arches, chassis, and potentially the entire underside.
- Angled Orientation: Sometimes, orienting the model at a slight angle (e.g., 15-30 degrees) can reduce the severity of overhangs and minimize the surface area touching the build plate, potentially improving adhesion.
Carefully consider which surfaces will be most visible and which can tolerate support marks. Evaluate the trade-offs between minimizing supports and ensuring a stable print.
Achieving Robust Bed Adhesion
A strong first layer is the foundation of any successful print. Common issues include:
- Nozzle Too High: The filament is extruded in a round bead, not squished onto the bed, leading to poor adhesion.
- Nozzle Too Low: Filament is scraped across the bed, causing clogs or uneven extrusion.
- Dirty Build Surface: Grease or dust from handling prevents filament from sticking. Clean your build plate regularly with isopropyl alcohol.
- Incorrect Bed Temperature: Different materials require specific bed temperatures (e.g., PLA: 50-60°C, PETG: 70-85°C).
- Warping: Large, flat areas can lift off the bed due to uneven cooling. Using a brim or raft in your slicer settings can increase the surface area adhering to the bed.
Leveling your print bed correctly and tuning your Z-offset are fundamental steps that cannot be skipped. A good first layer is essential for printing complex car models without them becoming detached.
5. Material Mismanagement and Printer Calibration
Using the wrong filament or failing to calibrate your 3D printer can lead to a cascade of printing problems, from weak layer adhesion to stringing and dimensional inaccuracy. Beginners often overlook the importance of material properties and printer tuning, assuming all filaments and printers behave identically.
Understanding Filament Properties
Different filament materials (PLA, PETG, ABS, TPU, etc.) have distinct characteristics affecting printability and final part properties. For car models:
- PLA: Easy to print, low warping, good for detailed models, but can be brittle and has a lower heat resistance. Often the best choice for beginners and display models.
- PETG: More durable and temperature resistant than PLA, but can be stringier and require slightly higher temperatures and slower speeds. Good for functional parts.
- ABS: Strong and temperature resistant, but prone to warping and requires an enclosure and good ventilation due to fumes. Less common for hobbyist car models unless high durability is needed.
Always check the manufacturer’s recommended print temperatures (nozzle and bed) and print speeds for each filament type. Storing filament in a dry environment is also crucial, as moisture absorption degrades print quality.
Essential Printer Calibration Steps
A well-calibrated printer is the bedrock of reliable 3D printing. Key calibration steps include:
- E-step Calibration: Ensures the printer extrudes the correct amount of filament.
- PID Tuning: Stabilizes nozzle and bed temperatures, preventing fluctuations that affect print quality.
- Flow Rate / Extrusion Multiplier: Fine-tunes the amount of filament extruded to prevent over- or under-extrusion, which is vital for accurate dimensions and clean surfaces on car models.
- Temperature Towers and Retraction Tests: Help determine the optimal temperature and retraction settings for a specific filament on your printer.
Regularly performing these calibrations, especially when switching filaments or noticing a decline in print quality, will save you from countless print failures and ensure your intricate car models come out perfectly.
6. Ignoring Layer Lines and Surface Finish
While layer lines are inherent to FDM 3D printing, beginners often accept them as an unavoidable flaw, leading to subpar surface finishes on their car models. For automotive replicas where smooth bodywork and crisp details are crucial, neglecting surface finish can significantly detract from the final aesthetic.
Minimizing Visible Layer Lines
Beyond using a finer layer height (0.1-0.15mm), several other techniques can help:
- Optimize Print Orientation: Orienting the model so that critical surfaces (like the car’s body panels) are printed with fewer “stair-stepping” effects from layer lines.
- Slower Outer Wall Speeds: Reducing the speed at which the outer perimeter is printed allows the filament more time to lay down smoothly.
- Vase Mode (Spiralize Outer Contour): While not suitable for most car models with complex internal structures, this mode can produce incredibly smooth continuous walls for simple, single-shell objects.
- Print Cooling: Adequate part cooling is essential for sharp details and preventing layer adhesion issues that can exacerbate visible lines, but too much cooling can reduce inter-layer adhesion.
Basic Post-Processing for a Smooth Finish
Even with careful printing, some layer lines might remain. Basic post-processing can dramatically improve the surface finish:
- Sanding: Start with coarser grit sandpaper (e.g., 120-220 grit) to remove major imperfections and layer lines, then progressively move to finer grits (400, 800, 1000+). Wet sanding can yield smoother results.
- Filling Primers: Applying a filler primer spray can fill in small imperfections and layer lines, creating a smooth surface for painting.
- Epoxy Resins/Fillers: For very smooth finishes, applying a thin coat of epoxy resin or using modeling putty can create a near-perfect surface.
Investing time in post-processing transforms a decent print into a professional-looking model, especially for detailed collectibles like those found on 88cars3d.com.
7. Overlooking Overhangs and Bridges
Car models are notorious for their complex aerodynamic shapes, which often translate to challenging overhangs (parts extending horizontally into open space) and bridges (horizontal spans between two supported points). Beginners frequently underestimate how these features will print, leading to droopy, stringy, or collapsed sections.
Understanding Overhang Limitations
Most FDM printers can handle overhangs up to a 45-degree angle without any support. Beyond that, gravity starts to pull the molten plastic down before it can solidify, causing sagging. Steep overhangs and perfectly horizontal extrusions (90 degrees) are impossible without support.
- Slicer Angle Settings: Most slicers allow you to define an “overhang threshold” or “support angle.” Any part of the model exceeding this angle can be flagged for support.
- Print Cooling: Excellent part cooling is critical for printing overhangs. It helps the extruded plastic solidify quickly, minimizing drooping. Ensure your cooling fan is running at an appropriate speed (often 100% for outer walls after the first few layers).
Tackling Bridges Effectively
Bridges are challenging because the filament is laid down with no support underneath until it reaches the other side. Success depends on:
- Slicer Bridge Settings: Slicers often have dedicated “bridge” settings that adjust print speed and cooling for these specific sections. Printing bridges slightly faster can sometimes help, as can increasing cooling.
- Filament Extrusion: Precise filament extrusion (flow rate calibration) is key. Over-extrusion can cause blobs that interfere with the bridge, while under-extrusion can lead to gaps.
- Support Interface: Using a support interface directly beneath the bridge can provide a solid surface for the bridge filament to adhere to, making it much cleaner.
For car models, components like spoilers, front splitters, and rear diffusers often present significant bridging and overhang challenges. Careful support placement and slicer tuning are essential.
8. Underestimating Small Details and Thin Walls
Many high-quality 3D printable car models, such as those available on 88cars3d.com, feature incredibly fine details: tiny vents, delicate spoilers, small emblems, or thin panel gaps. Beginners often run into trouble because their printer’s capabilities, filament diameter, or slicing settings aren’t optimized for such small features.
Nozzle Size and Layer Height Considerations
A standard 0.4mm nozzle can struggle with features smaller than its diameter. For extremely detailed models, consider:
- Smaller Nozzle: Switching to a 0.2mm or 0.25mm nozzle allows for finer detail reproduction. However, this significantly increases print time and requires recalibration of extruder steps and flow rate. It also makes the printer more susceptible to clogs from filament imperfections.
- Fine Layer Height: Using a layer height of 0.1mm or even lower is essential to capture the subtle curves and details without visible stair-stepping.
Wall Thickness and Minimum Feature Size
Ensure your slicer settings maintain adequate wall thickness for delicate features. Many slicers have a “minimum feature size” setting, but it’s often better to rely on the inherent geometry of the model and appropriate wall thickness settings. If a car model has very thin exhaust pipes or side mirrors, these might need to be thickened in a modeling program or by adjusting slicer settings (like wall line count) if they are too fragile after slicing.
- Wall Line Count: Increasing the number of walls (perimeters) can strengthen thin features without significantly increasing infill.
- Print Speed for Details: Slowing down print speeds considerably when printing these fine features allows the nozzle to trace them accurately.
Patience and precision are key. Sometimes, even with the best settings, a feature might be too small for a standard FDM printer to reproduce faithfully without supports. In such cases, consider the capabilities of your printer and the model’s design.
9. Ignoring Resin Printing Specifics (If Applicable)
While FDM is common, many highly detailed car models are also offered for resin printing (SLA/DLP/MSLA). Beginners venturing into resin printing often make mistakes specific to this technology, which differs significantly from FDM.
Understanding Resin Properties and Safety
Resin is a liquid photopolymer that hardens when exposed to UV light. It’s messy, requires careful handling, and proper safety precautions (gloves, ventilation, eye protection) are non-negotiable. Different resin types (standard, tough, flexible, castable) have varying properties and require specific exposure times.
Support Structures and Orientation for Resin
Resin printing requires supports that are much finer and more numerous than FDM supports. They are crucial for preventing layer separation (suction forces) and ensuring adhesion to the build plate.
- Light Supports: Use light, fine supports, often with a small tip size (e.g., 0.2-0.4mm).
- Heavy Supports: Use heavier supports for larger, heavier features or areas prone to suction.
- Orientation is Key: Orient models to minimize the surface area exposed during each layer’s cure time, especially on the initial layers. Angling the model at 15-45 degrees often helps reduce suction forces and improve print success. Avoid large, flat surfaces parallel to the build plate.
- Hollowing Models: For larger resin prints, hollowing the model and adding drainage holes is essential to reduce material waste, print time, and prevent internal pressure buildup during curing and washing.
Washing and Curing Process
After printing, resin models must be thoroughly washed (typically in isopropyl alcohol or a specialized wash solution) to remove uncured resin, and then cured under UV light to achieve their final hardness. Incomplete washing or curing leads to sticky, weak prints. Beginners often rush these steps or fail to understand the importance of proper post-processing for resin prints.
10. Skipping Test Prints and Calibration Models
Perhaps the most common mistake is jumping straight into printing a large, complex car model without first verifying the printer’s settings and capabilities. This often results in a partially printed, failed, or subpar model that can be disheartening.
The Value of Calibration Prints
Before committing to a multi-hour print of a detailed car model, always run small, targeted calibration prints. These help you dial in specific settings:
- Temperature Towers: Test different temperature settings for a filament to find the optimal range for layer adhesion and bridging.
- Retraction Tests: Fine-tune retraction distance and speed to eliminate stringing.
- Overhang Test Cubes: Verify your printer’s ability to handle various overhang angles with your current settings.
- Small Detail Tests: Print small objects with fine details (like calibration miniatures or small parts of the car) to check nozzle performance and layer consistency.
- Bed Leveling Tests: Print a large square or multiple small squares across the build plate to ensure a perfect first layer everywhere.
Iterative Improvement
3D printing is an iterative process. Don’t expect perfection on the first try. Use calibration prints to make small adjustments to your slicer settings (e.g., +/- 5°C temperature, +/- 1mm retraction, +/- 5 mm/s speed). Once you achieve satisfactory results on these small tests, then proceed to your chosen car model. This methodical approach saves significant time, material, and frustration in the long run.
Conclusion: Your Path to Flawless Car Model Prints
Bringing intricate 3D car models to life through printing is an incredibly rewarding experience, but it requires more than just hitting the “print” button. By understanding and actively avoiding these ten common beginner mistakes – from neglecting file preparation and mastering slicer settings to properly managing supports, bed adhesion, materials, and calibration – you can dramatically elevate the quality of your prints. Whether you’re printing a classic beauty or a race-ready machine, paying attention to detail in every step, from downloading print-ready STL files from sources like 88cars3d.com to the final post-processing, will yield spectacular results. Embrace the learning process, utilize calibration prints, and be patient. Each successful print builds your expertise, paving the way for increasingly complex and stunning automotive creations from your 3D printer.
“`
Featured 3D Car Models
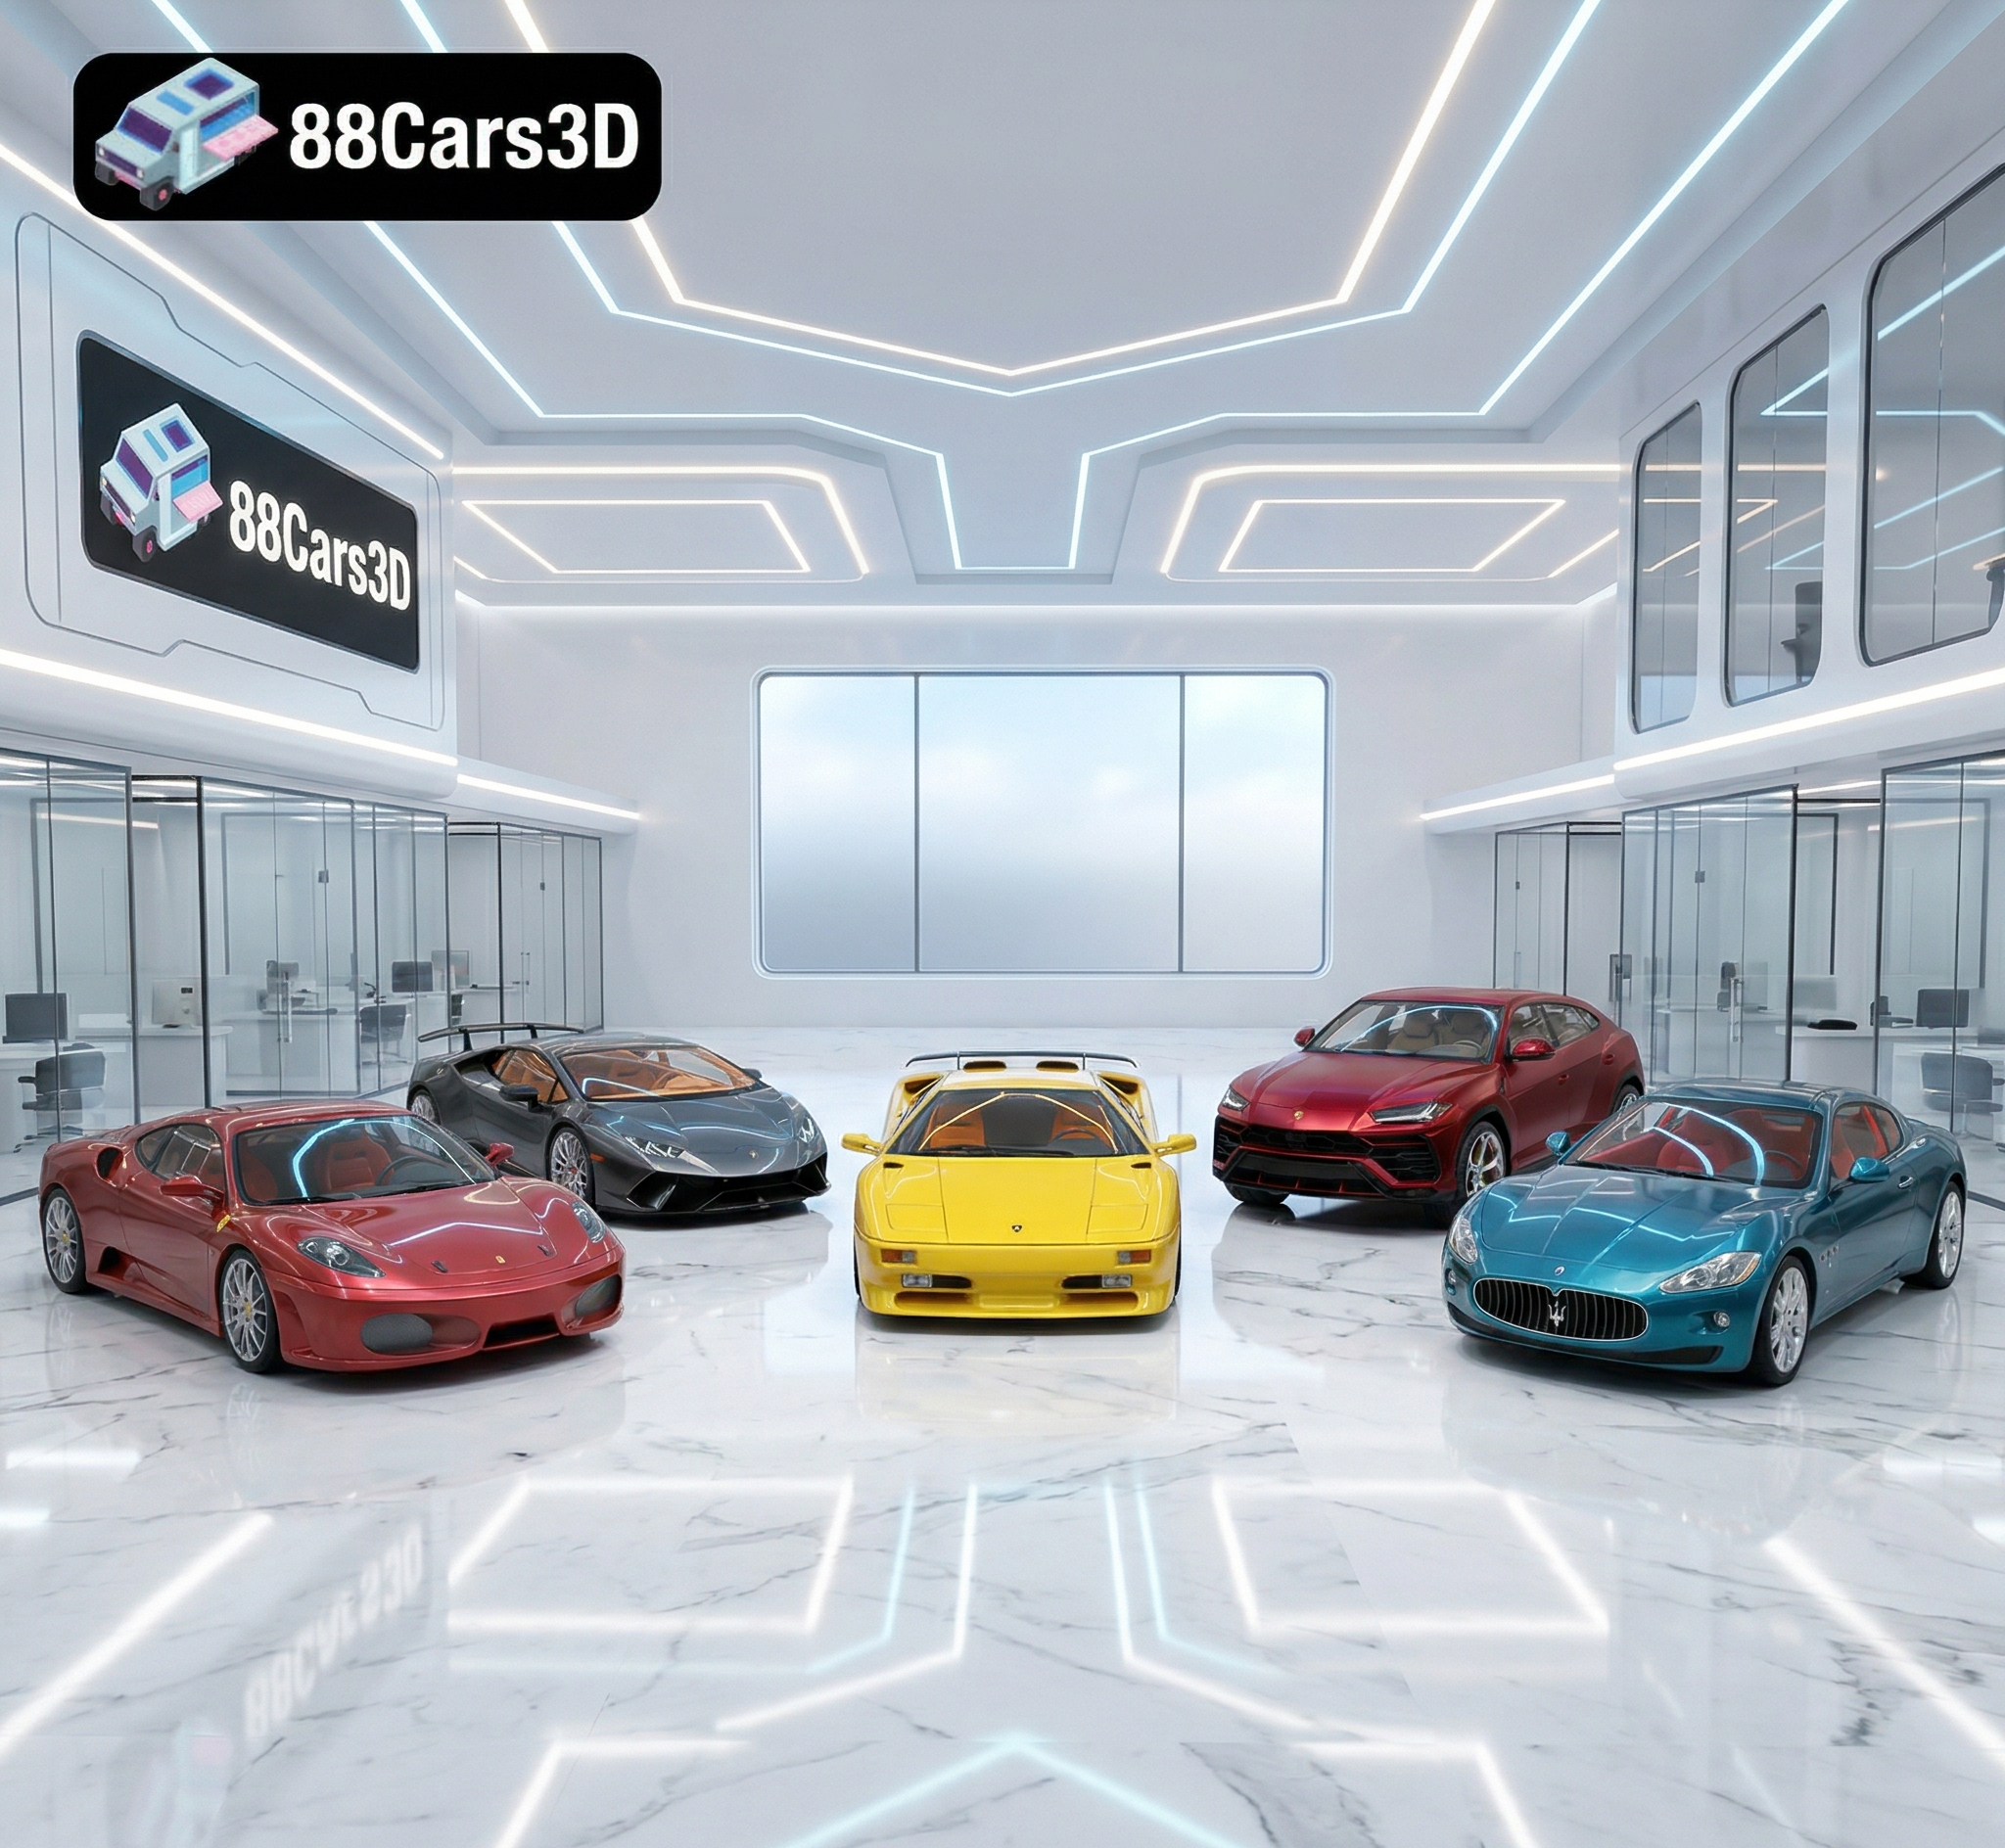
The Italian Legends Bundle 5 Ultimate Supercar 3D Models STL Optimized
Texture: Yes | Material: Yes | 3D Printable: Yes. Download the Italian Thoroughbreds Bundle featuring 5 iconic 3D models: Lamborghini Huracán Performante, Ferrari 458 Italia, Lamborghini Urus, Diablo SV, and Maserati GT. Optimized for 4K rendering and 3D printing (STL included). Save 50% with this ultimate Italian vehicle collection.
Price: $199.99

Elite Future Mobility: EV & Autonomous SUV Bundle (4 High-End 3D Models)3D Printable STL
Download the Elite Future Mobility Bundle featuring 4 highly optimized 3D models: Tesla Model S, Avatr 11, Li L9, and Zoox Robotaxi. Perfect for ArchViz, Smart City renders, and game dev. Optimized for Unreal Engine and Blender. Includes .fbx, .obj, and .max formats.
Price: $99
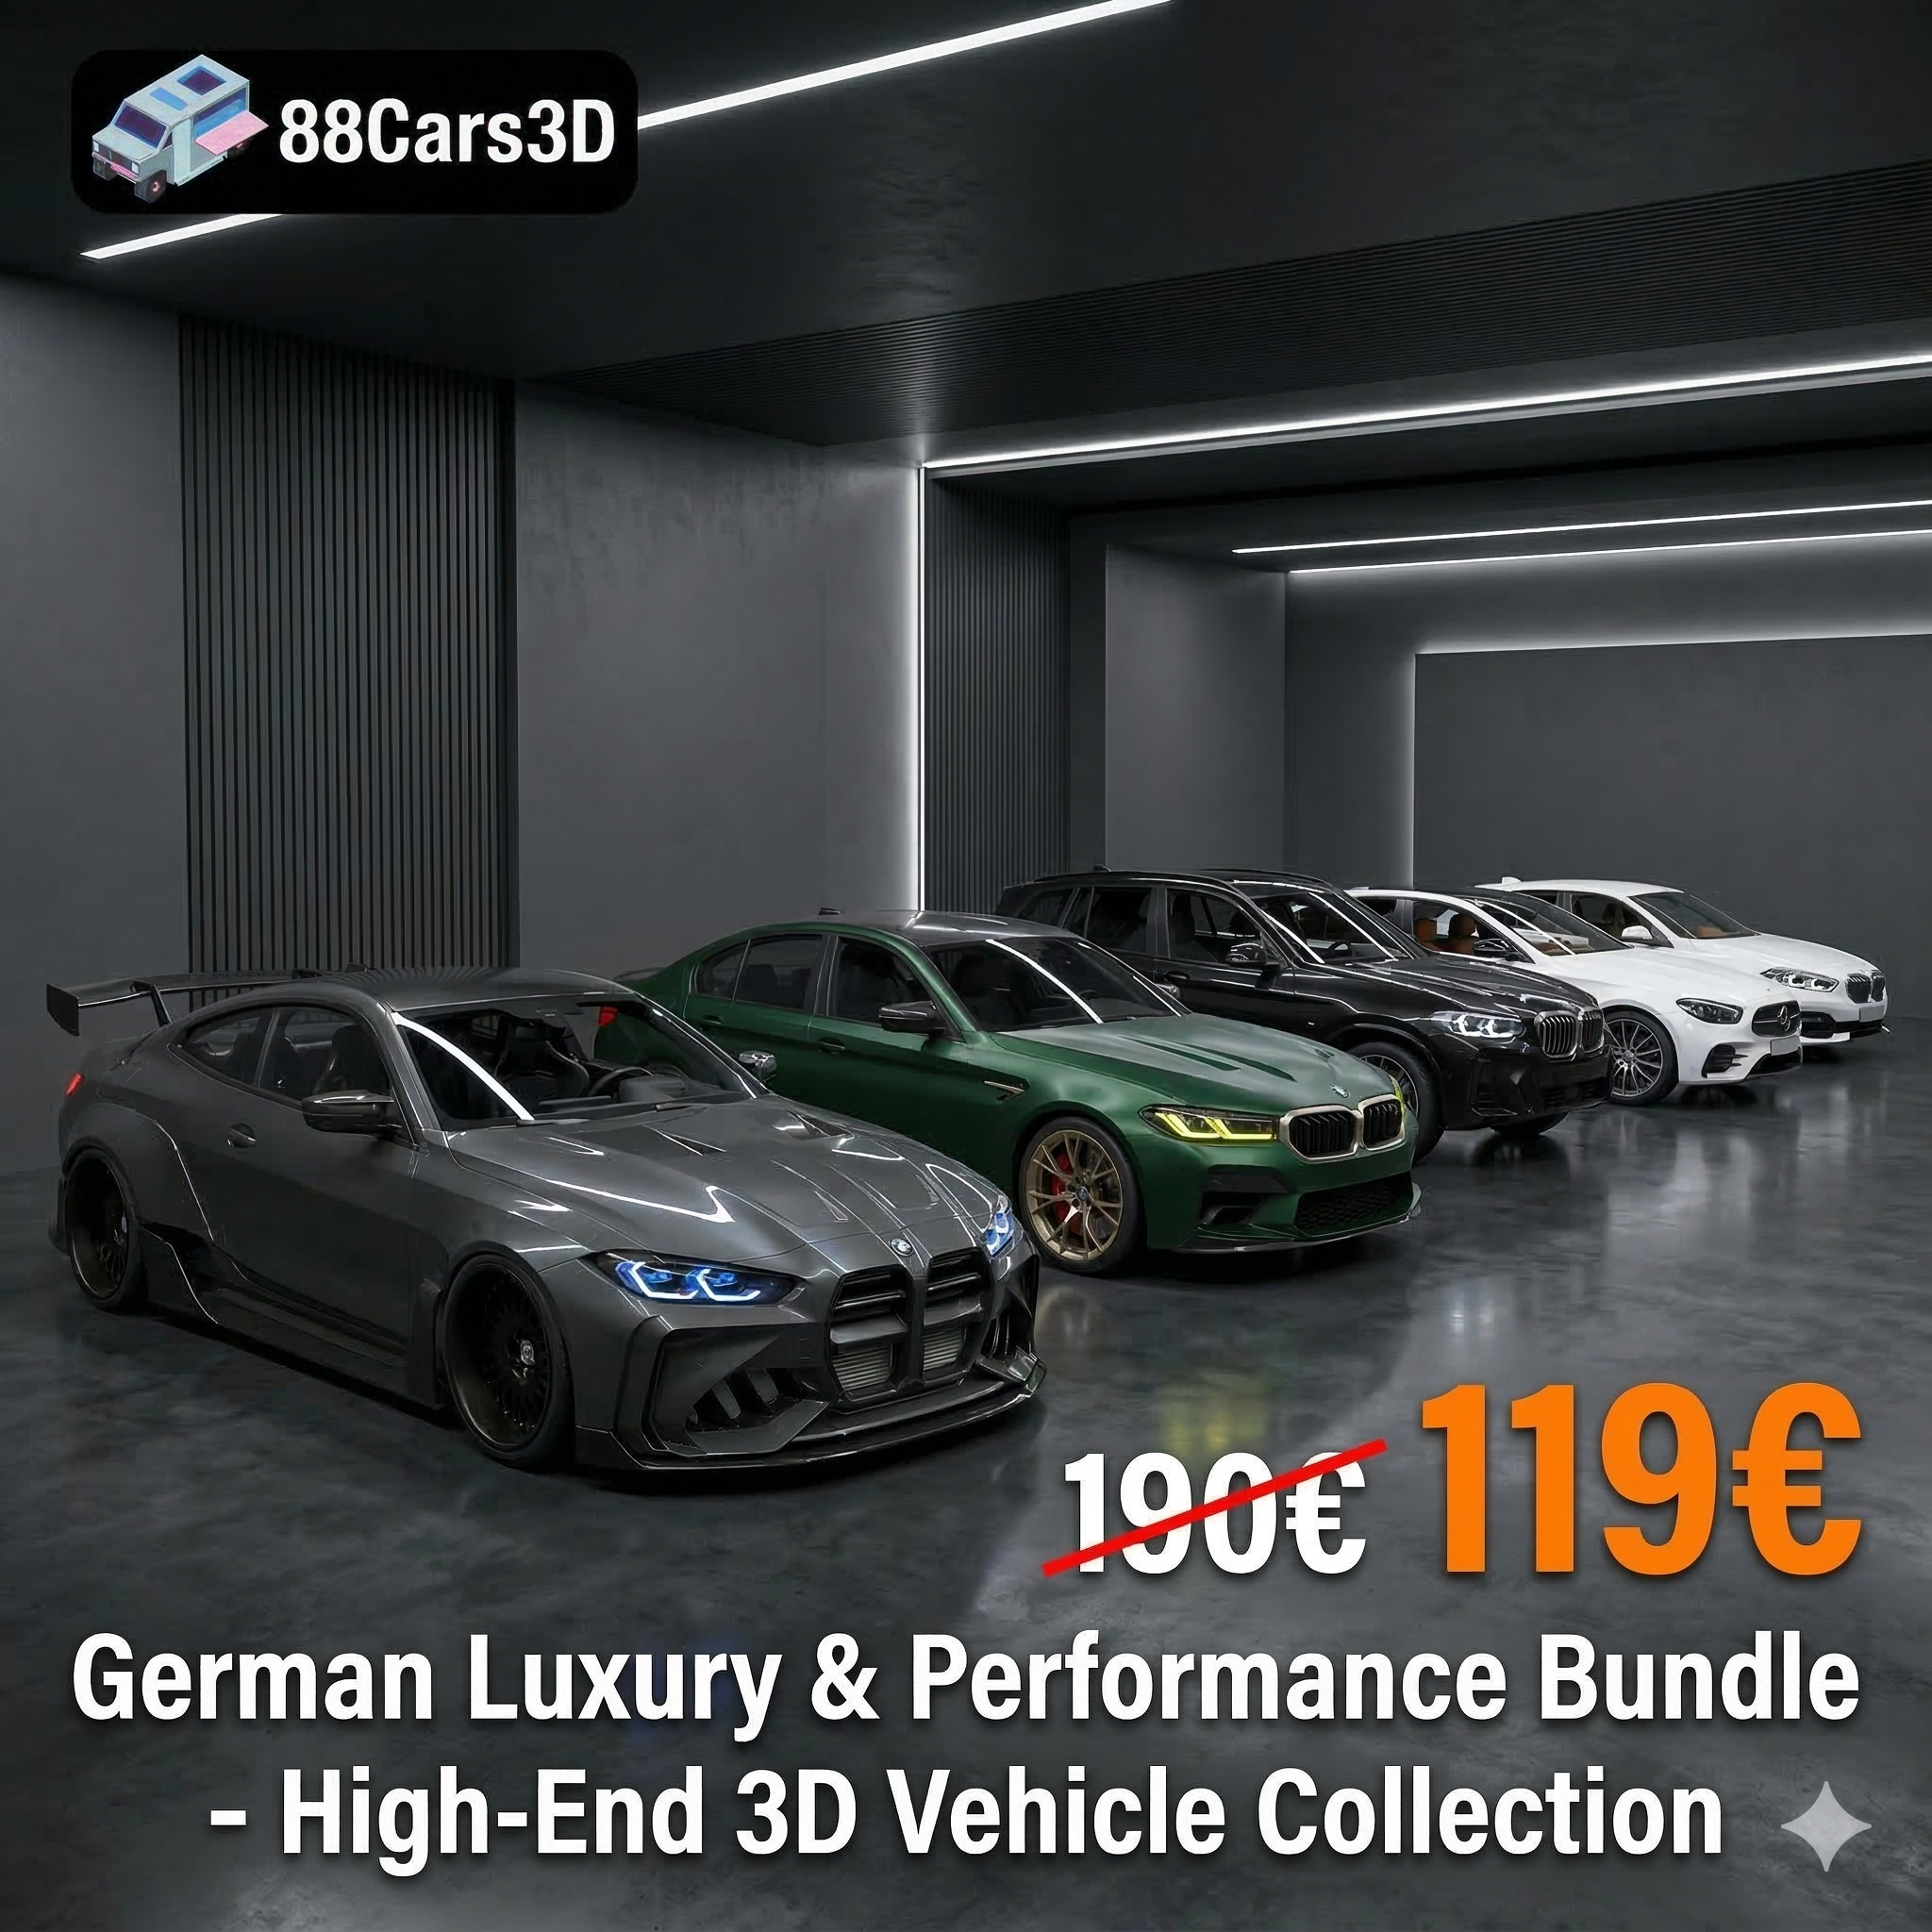
German Luxury & Performance Bundle – High-End 3D Vehicle Collection3D Printable STL
🚗 5 Iconic German Cars (BMW M4 G82, M5 CS, X3, 1 Series & Mercedes E-Class). ✅ Optimized for ArchViz: Ready for Corona & V-Ray. 💰 Save €71 with this limited-time collection! 🚀 Instant Download after purchase.
Price: $119
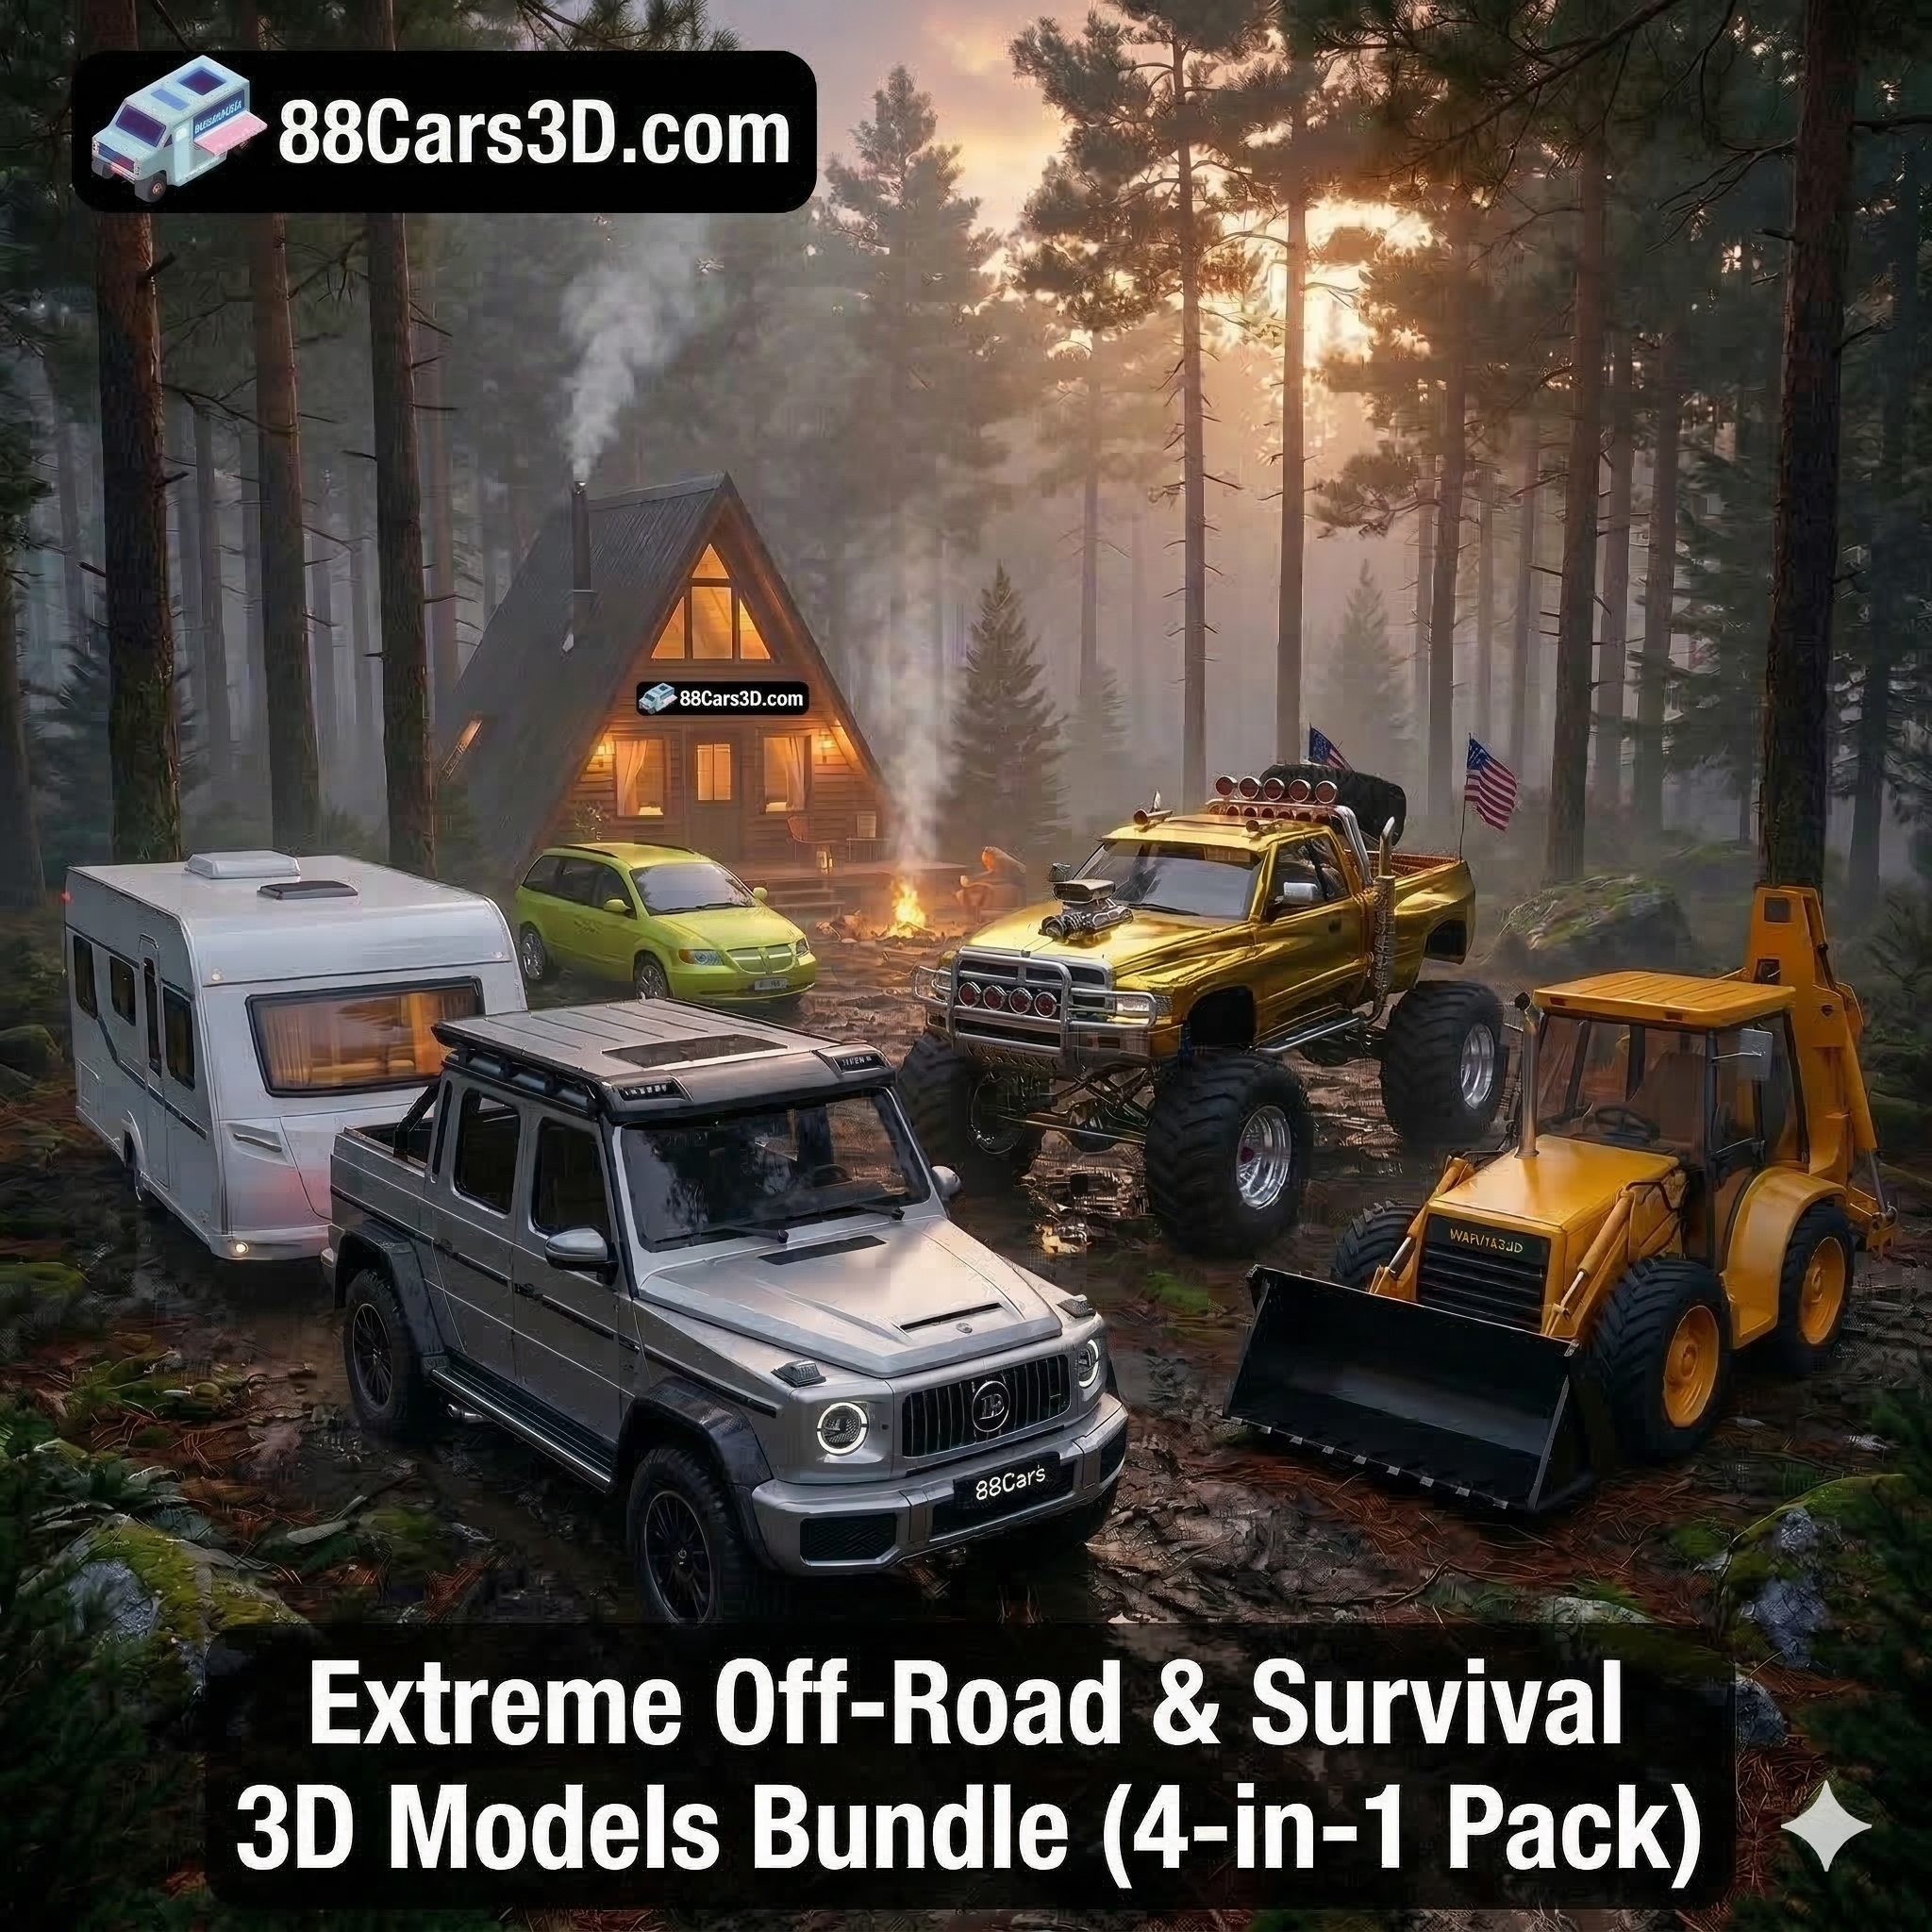
Extreme Off-Road & Survival 3D Models Bundle (4-in-1 Pack)3D Printable STL
Download the Extreme Off-Road & Survival 3D Models Bundle! Includes the Brabus 800 Adventure, Dodge Ram Bigfoot, Spec Truck, and a Caravan. Save over €210 on this premium 4-in-1 off-grid vehicle pack for ArchViz and game development.
Price: $149.99
Heavy Duty & Commercial Logistics 3D Models Bundle (4-in-1 Pack)3D Printable STL
Download the Heavy Duty & Commercial Logistics 3D Models Bundle! Includes the Ford Sterling, Caterpillar CT680, Mercedes Citaro Bus, and Vito Van. Save over €130 on this massive, game-ready 4-in-1 industrial vehicle pack.
Price: $109.99

The Ultimate Garage Props & Custom Motorcycles 3D Models Bundle 3D Printable STL
Download the Ultimate Custom Motorcycles 3D Models Bundle. Includes a Custom Chopper, Ducati 916 Café Fighter, Harley XR1200X, and BMW K100. Perfect premium props for luxury ArchViz garages. Save over €250 today!
Price: $159.99

Japanese Legends: JDM Street Racing 3D Models Bundle (5-in-1 Pack) Nissan Mitsubishi Honda Mazda Toyota 3D Printable STL
Download the ultimate JDM Street Racing 3D Models Bundle! Includes the Nissan GT-R, Toyota Supra, Mazda RX-7, Lancer Evo IX, and Honda NSX. Save big on this highly optimized, game-ready 5-in-1 Japanese legend car pack.
Price: $129.99

American Muscle & Classics Pack 4 in 1 Ford Dodge Chevrolet 3D Printable STL
Download the ultimate American Muscle & Cinematic Classics 3D Models Bundle! Includes the Dodge Charger ’68, Mustang Eleanor GT500, Camaro Z28 ’79, and a custom ’69 Mustang. Save over €240 on this game-ready, premium 4-in-1 pack.
Price: $149.99
Everyday City Traffic Essentials pack 5in1 Hyundai Kia Volkswagen Toyota Ford 3D Printable STL
Download the Everyday City Traffic 3D Models Bundle. Includes the VW Golf, Kia Picanto, Hyundai Tucson, Toyota Yaris, and a DHL Ford Transit Van. Save big on this 5-in-1 pack, perfectly optimized for realistic ArchViz streets and game traffic.
Price: $99.99
The Future of Mobility: Smart City EV 3D Models Bundle (5-in-1 Pack) Volvo Tesla AVATR Porsche 3D Printable STL
Download the Future of Mobility EV 3D Models Bundle. Includes the Volvo EX30, Tesla Model S, AVATR 11, Porsche Taycan, and a Siemens EV Charger. Save big on this highly optimized 5-in-1 pack for ArchViz and game development!
Price: $89.99
